



Tiêu chí tân trang dụng cụ máy tính bảng: Sửa chữa, Phủ lại, hoặc Thay thế
Tablet tooling refurbishment criteria should separate three very different conditions. Minor surface damage may be repairable. A worn functional coating may justify recoating when the underlying tool remains sound. Vết nứt, lost geometry, deep pitting, or dimensions outside approved limits usually point toward replacement.
The decision applies to tablet compression punches and dies, not to electronic-tablet tools. Readers who need broader context on tooling configurations can first review Các loại dụng cụ ép viên. This guide stays focused on the condition assessment that determines whether existing tooling can return to service.
No single public wear limit applies to every punch or die. The final acceptance basis should come from the approved drawing, tooling specification, internal SOP, validated process requirements, and the measured history of the tooling set.
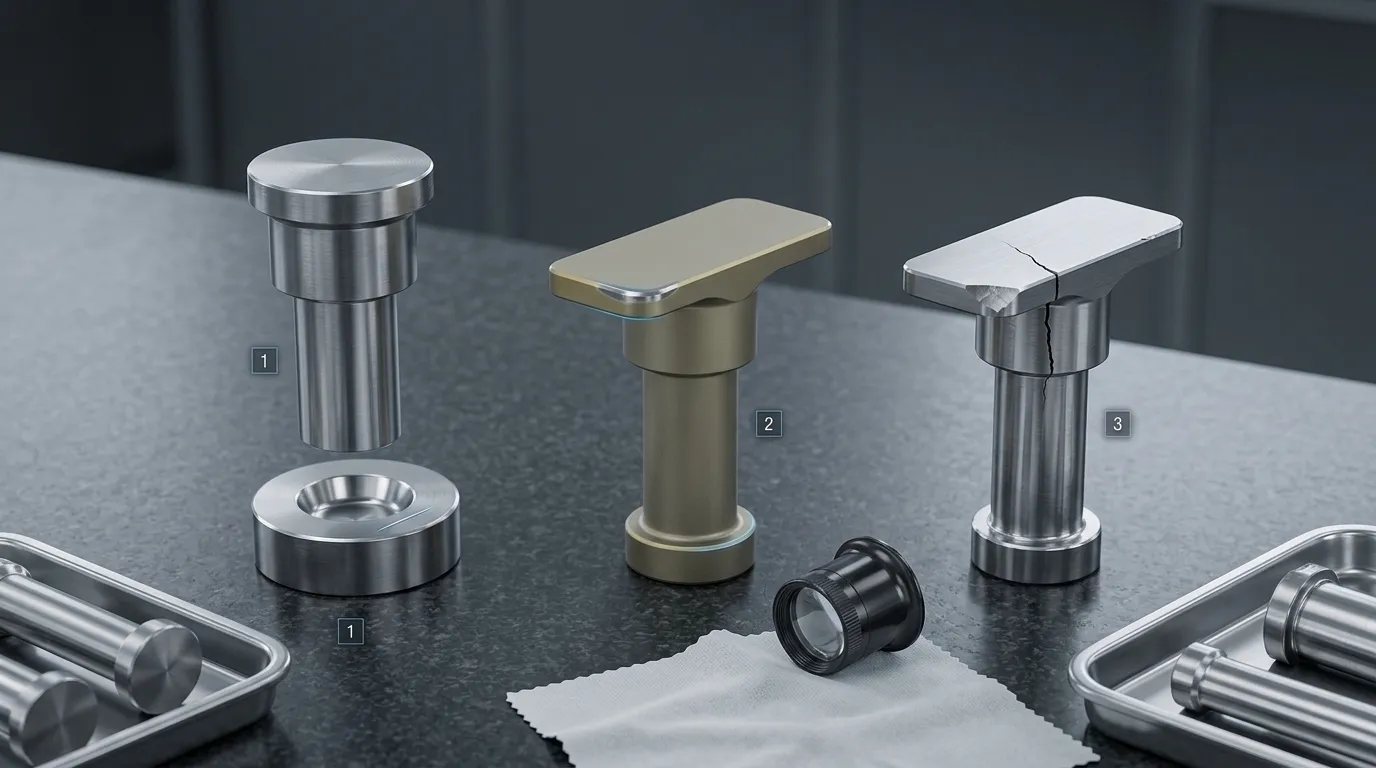
Sửa chữa, Phủ lại, hoặc Thay thế: The Decision at a Glance
A visible defect does not automatically determine the correct action. The location, Độ sâu, remaining geometry, điều kiện nền tảng, coating history, and effect on the complete tooling set all matter.
| Điều kiện quan sát được | Sắp xếp có thể xảy ra | Yêu cầu xác minh | Lý do |
|---|---|---|---|
| Light burr, shallow scratch, small nick, early J-hook, or limited surface corrosion | Có thể sửa chữa có kiểm soát | Kiểm tra phóng đại và kiểm tra kích thước trước và sau khi loại bỏ vật liệu | Hư hỏng bề mặt nhỏ có thể được loại bỏ mà không làm mất hình học quan trọng |
| Mòn, bị hư hại, or partially detached coating with sound base material | Có thể xem xét sơn lại | Coating removal assessment, substrate inspection, kiểm tra kích thước, and post-coating inspection | Lỗi có thể giới hạn ở bề mặt chức năng |
| Lost land, altered cup profile, excessive working-length variation, or die-bore wear outside approved limits | Thay thế hoặc nhận được đánh giá của chuyên gia | Comparison with the approved drawing, thông số kỹ thuật, and set measurements | Lớp phủ hoặc đánh bóng không thể xây dựng lại hình học bị thiếu |
| Vết nứt, severe chip, deep pitting, biến dạng, or uncertain structural integrity | Thay thế | Hồ sơ từ chối và xem xét nguyên nhân gốc rễ | Continued use may increase breakage, Sự ô nhiễm, and tablet-quality risks |
| Tình trạng không thể được đo lường hoặc truy xuất một cách đáng tin cậy | Giữ lại để chuyên gia xem xét hoặc thay thế | Confirm tool identity, chỉnh sửa bản vẽ, Vật chất, Lớp phủ, and maintenance history | Một công cụ không được quay trở lại sản xuất khi không thể chứng minh được sự phù hợp |
“Specialist review” is a valid disposition. Maintenance teams should not force an uncertain tool into a repair or replacement category before the necessary measurements and material assessment are available.
Thiết lập bằng chứng trước khi đưa ra quyết định
The condition of a punch or die should be documented before polishing, gia công, coating removal, or any other operation changes the evidence.
A controlled assessment normally follows this sequence:
- Segregate and identify the tooling. Record the tool number, set, vị trí, Vật chất, Lớp phủ, chỉnh sửa bản vẽ, and production batch or campaign where the issue appeared.
- Clean and dry the components. Residue can hide corrosion, tính điểm, coating failure, and fine cracks.
- Review the service history. Check previous polishing, các sửa chữa, working-length corrections, coating cycles, and recurring defects.
- Conduct visual and magnified inspection. Examine tablet-forming surfaces, contact surfaces, guidance areas, chìa khóa, edges, và chết chán.
- Measure critical dimensions. Use calibrated instruments and an approved inspection method.
- Compare each component with the specification and the set. A tool can pass an isolated dimensional check but still create inconsistency if it no longer matches the rest of the set.
- Assign a provisional disposition. Sửa chữa, recoat, specialist review, hoặc thay thế.
- Record the original condition. Photographs and before-service measurements help establish what work was performed and how much material was removed.
In regulated drug manufacturing, equipment cleaning and maintenance should follow written procedures under 21 CFR 211.67. Measuring devices should also be controlled under an appropriate calibration program, as addressed by 21 CFR 211.160. These requirements do not provide punch or die wear limits, but they support controlled inspection, documented responsibilities, and reliable measurements.
Treat Tablet Defects as Inspection Triggers, Not Proof
Dính, việc hái, nắp, cán màng, nhấp nháy, difficult ejection, or inconsistent tablet dimensions can justify a tooling inspection. They do not prove that worn tooling is the sole cause.
Tablet defects may also involve:
- tính chất công thức;
- granulation condition;
- lubricant distribution;
- tablet shape and embossing;
- compression force;
- nhấn cài đặt;
- hiệu suất cấp liệu;
- thời gian ở lại;
- environmental conditions.
Research on punch-surface evolution shows that sticking behaviour can depend on the powder, compression conditions, run length, and punch-surface quality rather than one isolated factor. The study is indexed in PubMed. A broader technical review of tablet scoring and manufacturing defects also describes the interaction among formulation, design, Dụng cụ, and process variables in Khoa học ứng dụng.
Production symptoms should guide the inspection location. They should not replace dimensional measurement or root-cause analysis.
Use the Correct Drawing, Đặc điểm kỹ thuật, and Tool History
Các tài liệu tham khảo chính xác phải được xác định trước khi bất kỳ ai quyết định rằng một công cụ "nằm trong khả năng chịu đựng".
The assessment record should confirm:
- tooling format and component type;
- unique tool or set identification;
- bản vẽ và chỉnh sửa đã được phê duyệt;
- specified material;
- coating type and history, nếu có;
- required critical dimensions;
- internal acceptance limits;
- previous repair or rework;
- previous coating removal and recoating;
- recorded production or maintenance problems.
Generic internet values should not replace approved limits. Even tools that appear similar may have different cup geometry, chiều rộng đất, chiều dài làm việc, cấu hình đầu, Lớp phủ, hoặc yêu cầu ứng dụng.
The service history is particularly important because every polishing or machining operation may remove material. A component that tolerated one minor repair may have less restoration margin after several earlier interventions.
Khi sửa chữa có kiểm soát có thể thích hợp
Controlled repair is most appropriate when damage is limited, dễ tiếp cận, and removable without taking the component outside its approved geometry.
Potentially repairable conditions may include:
- small burrs;
- shallow scratches;
- minor nicks;
- light surface corrosion;
- early J-hook formation;
- slight surface deterioration;
- localized roughness that has not penetrated deeply into the substrate.
These descriptions are not automatic approval criteria. A shallow scratch on a non-critical area may be less serious than a similar mark across the punch cup, đất đai, key, or die bore.
The technician must consider:
- defect depth;
- defect location;
- amount of material that must be removed;
- remaining land or edge geometry;
- hình dáng cốc;
- chiều dài làm việc;
- coating status;
- effect on the tooling set.
Controlled polishing can remove minor imperfections, but it also removes tool material. Hướng dẫn kỹ thuật từ Công nghệ dược phẩm recommends inspection, sửa chữa, phép đo, and polishing as separate stages rather than treating polishing as the entire maintenance process. Hướng dẫn bảo dưỡng đục lỗ của Natoli also warns that unnecessary refurbishment removes material and that not every wear condition is repairable.
The goal is not to make a component look new. The goal is to remove the defect while preserving approved geometry and function.
Những gì phải được kiểm tra lại sau khi vật liệu được loại bỏ
Any repair that removes material should be followed by another inspection.
Depending on the affected component, this may include:
- punch working length;
- cup depth and profile;
- embossing condition;
- land width and continuity;
- punch-tip shape;
- head-flat condition;
- head angle;
- barrel condition;
- key or orientation feature;
- Kích thước nòng die;
- consistency with the rest of the set.
Before-and-after measurements should be retained in the tooling history. A visually smooth surface is not enough if the repair has altered the cup, shortened the punch, reduced the land excessively, or created variation across the set.
Khi lớp phủ lại có thể bảo vệ được về mặt kỹ thuật
Recoating should be considered only when the functional coating is the main failure and the underlying tool remains suitable for service.
Possible coating-related evidence includes:
- hao mòn cục bộ;
- coating delamination;
- reduced surface performance;
- nền trần;
- coating damage from handling or service;
- deterioration that contributes to friction or product adhesion.
Before recoating, the assessment should answer five questions.
- Can the existing coating be removed without damaging the tool?
The stripping process must be compatible with the substrate, hình học, and existing surface condition. - Is the substrate structurally sound?
The tool should be checked for cracks, severe corrosion, deep pitting, biến dạng, and hidden damage beneath the coating. - Do the critical dimensions still conform?
Coating renewal should not be used to disguise lost land, hình học cốc thay đổi, excessive working-length variation, or die-bore wear. - Is the replacement coating compatible with the application?
Vật chất, hành vi công thức, điều kiện vận hành, and the original tooling specification may affect the choice. - Can the finished tool be verified after recoating?
Tình trạng bề mặt, coating coverage, affected dimensions, and set consistency should be inspected before release.
A refurbishment supplier may use coating removal, chuẩn bị bề mặt, and coating application as separate controlled stages. The exact process and acceptance method should be confirmed with that supplier. SunshinePro’s published website does not verify that it offers coating stripping or recoating, so those services should not be assumed.
Những gì sơn lại không thể sửa chữa
Recoating changes the functional surface. It does not rebuild missing base material.
It cannot correct:
- a cracked punch or die;
- a severely chipped edge;
- deep substrate pitting;
- lost cup geometry;
- an excessively reduced land;
- unacceptable working-length variation;
- a deformed head or barrel;
- a damaged key;
- die-bore geometry outside approved limits;
- uncertain substrate integrity.
A new coating over a nonconforming substrate may improve appearance while leaving the underlying failure unresolved.
Các điều kiện hướng tới sự thay thế
Replacement becomes the stronger technical choice when a component cannot be restored and verified without compromising its function or safety.
Common replacement indicators include:
- visible or suspected cracking;
- sứt mẻ nặng;
- missing material;
- deep corrosion or pitting;
- biến dạng;
- unacceptable working length;
- irrecoverable cup or embossing geometry;
- excessive land loss;
- severely worn head or barrel features;
- damaged orientation keys;
- die-bore wear outside approved limits;
- recurring failure after previous repair or recoating;
- unknown material or coating history;
- inability to identify the correct drawing or acceptance specification.
The seriousness of a defect also depends on its position. Damage on a tablet-forming surface may affect tablet appearance, Phát hành, or dimensional consistency. Damage on a punch head, thùng rượu, or key may affect movement, sự căn chỉnh, or interaction with the press. Die-bore damage can influence compression, sự đẩy ra, nhấp nháy, and tablet integrity.
Technical suitability should be decided before cost. A low repair quotation does not make a structurally damaged or dimensionally nonconforming tool acceptable.
Xem xét toàn bộ bộ dụng cụ và lịch sử tân trang của nó
A punch or die should not always be judged in isolation.
One repaired punch may create set-level variation if its:
- working length differs from the others;
- cup depth has changed;
- land has been altered;
- head geometry no longer matches;
- coating thickness or surface condition differs;
- prior repair history is substantially different.
The complete tooling record should show how many times each component has been polished, được gia công, corrected, or recoated. There is no universal safe maximum number of refurbishments. One light repair may remove less material than another aggressive intervention.
Recurring damage may also indicate a wider unresolved issue, such as press alignment, Xử lý, việc dọn dẹp, Lưu trữ, formulation abrasiveness, corrosive exposure, or excessive operating load. Replacing the tool without investigating the cause may only restart the same failure cycle.
Đánh giá các cú đấm và chết theo các tính năng quan trọng của chúng
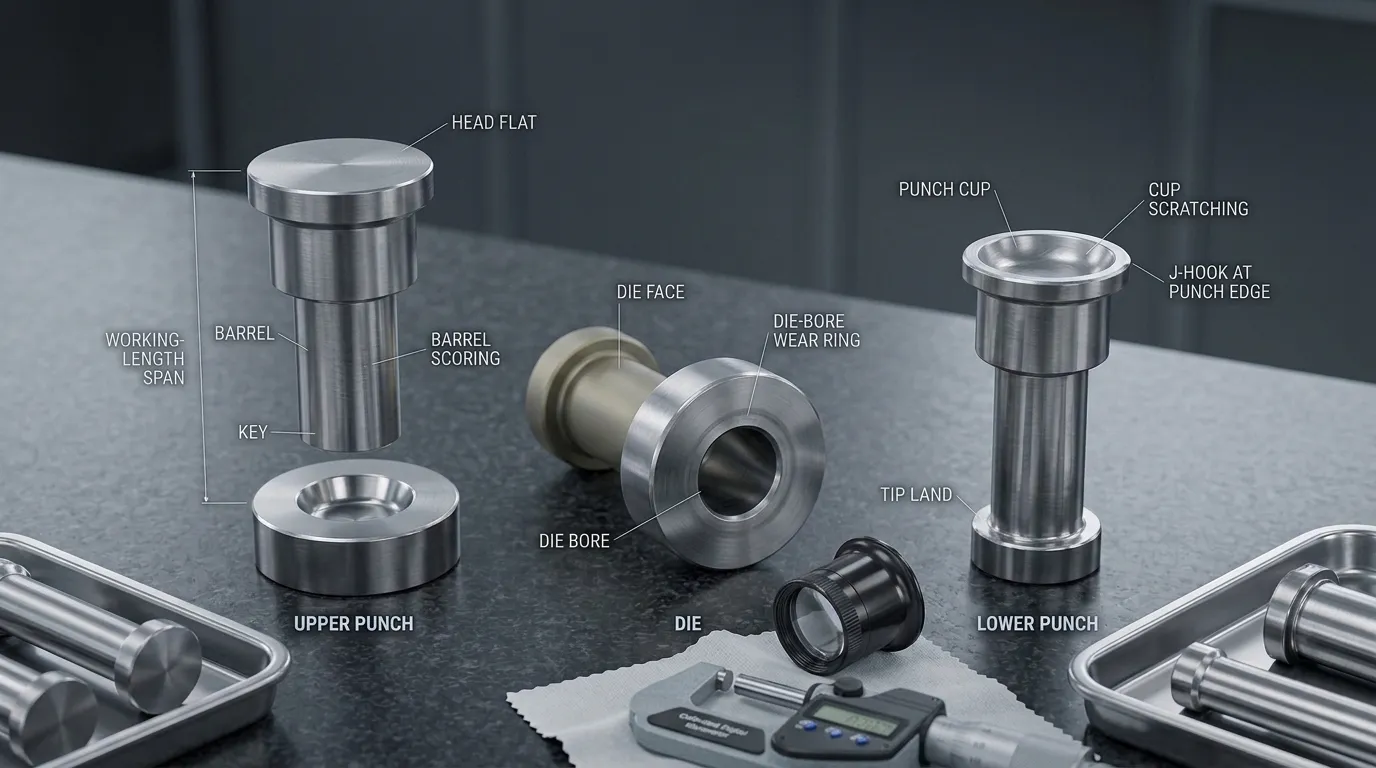
Different tooling features perform different functions. The inspection should therefore connect each defect to the feature it affects.
| Đặc tính | Điều kiện để xem xét | Tại sao điều này lại quan trọng |
| Cốc đục lỗ và dập nổi | Vết xước, đang làm rỗng, coating loss, profile damage, filled or rounded detail | Các bề mặt này tạo thành mặt và dấu hiệu của máy tính bảng |
| Vùng đất đầu đục lỗ | Lưỡi gờ, J-hook, uneven width, mẻ, material loss | Land condition can affect tablet edges, Phát hành, and structural behaviour |
| Chiều dài làm việc | Thay đổi so với giới hạn đã được phê duyệt hoặc bộ dụng cụ | Sự không nhất quán về chiều dài làm việc có thể ảnh hưởng đến độ nén và tính nhất quán của viên nén |
| Đầu đục lỗ và đầu phẳng | Mặc, biến dạng, tính điểm, altered contact surface | Các khu vực này tương tác với các bộ phận ép và ảnh hưởng đến sự truyền lực |
| Thùng đục lỗ | Scoring, sự ăn mòn, excessive wear, biến dạng | Tình trạng thùng ảnh hưởng đến hướng dẫn và chuyển động |
| Tính năng chính hoặc định hướng | Mặc, sự lỏng lẻo, thiệt hại, incorrect position | Tính năng định hướng điều khiển căn chỉnh cú đấm |
| Khuôn mặt | Handling damage, sự ăn mòn, khoai tây chiên, các gờ | Tổn thương khuôn mặt có thể ảnh hưởng đến việc lắp đặt và căn chỉnh |
| Lỗ khoan | Đeo nhẫn, tính điểm, sự ăn mòn, thuôn dần, surface deterioration | Bore condition affects tablet formation, sự nén, và đẩy ra |
Các tính năng Punch để đánh giá
The punch cup, Dập nổi, đất đai, chiều dài làm việc, đầu, thùng rượu, and key should be assessed separately.
A small surface mark in the cup may be repairable if it can be removed without changing the profile. A chipped embossing feature or deeply pitted cup may require replacement because the tablet-forming geometry cannot be recreated reliably through polishing.
Early J-hook development at the punch edge may sometimes be corrected through controlled restoration. Severe edge loss is different. Removing enough material to eliminate it may reduce the land or alter the tablet profile.
Head and barrel defects should not be ignored simply because they do not contact the tablet. These features control how the punch moves and interacts with the press. Scoring, biến dạng, or wear can affect alignment and loading.
Các tính năng của Die để xem xét
The die bore should be checked for:
- wear rings;
- tính điểm;
- sự ăn mòn;
- đang làm rỗng;
- taper or dimensional change;
- độ thô ráp;
- localized coating failure;
- damage near the entry or compression zone.
Die-bore wear may contribute to poor ejection, nắp, nhấp nháy, và sự không nhất quán về kích thước, but measurement is required before assigning the cause. The detailed metrology process belongs in a dedicated guide to máy tính bảng đo độ mòn lỗ khoan.
The die face and external installation surfaces should also be inspected for burrs, handling damage, and deformation that may affect seating or alignment.
Xác minh dụng cụ tân trang trước khi quay trở lại sản xuất
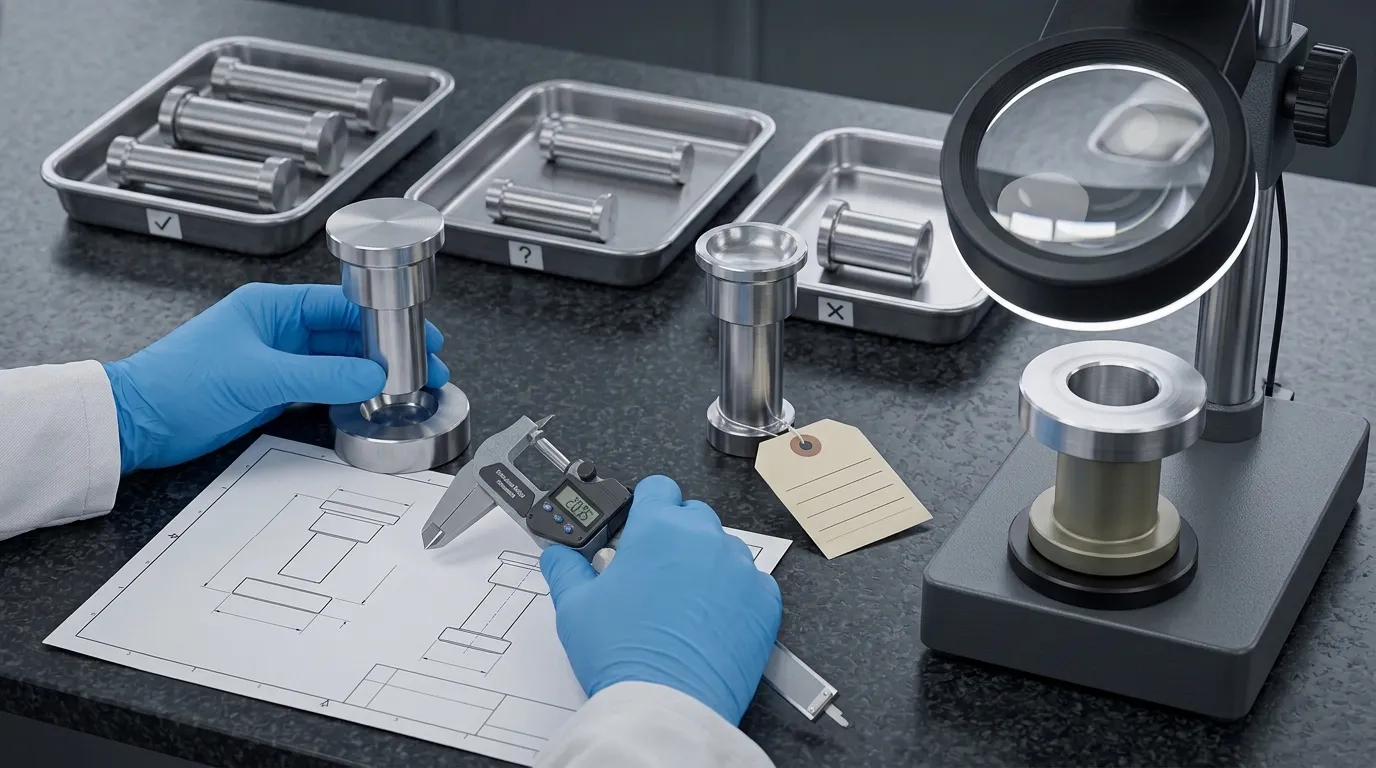
A completed repair or coating operation is not the same as release approval. The affected tool should be inspected again after the work is finished.
A practical release checklist includes:
- repeat visual and magnified inspection;
- verify that the original defect has been removed or controlled;
- measure all affected critical dimensions;
- compare the component with the approved specification;
- compare the component with the rest of the tooling set;
- inspect repaired edges, đất đai, Cốc, mặt ngửa, các thùng, chìa khóa, and die bores as applicable;
- confirm coating coverage and surface condition where recoating was performed;
- verify cleanliness and corrosion protection;
- record the work completed;
- record before-and-after dimensions;
- identify the technician and approver;
- document the final disposition.
For regulated pharmaceutical operations, 21 CFR 211.182 addresses chronological equipment cleaning and maintenance records. Thuộc tính Khung EU GMP Tập 4 also supports controlled equipment, Tài liệu, Sản xuất, and quality-system practices.
These sources establish the need for controlled procedures and records. They do not establish a universal acceptable scratch depth, chiều rộng đất, chiều dài làm việc, or die-bore limit. Those limits must come from the applicable technical documentation and approved quality system.
Đánh giá nhà cung cấp tân trang hoặc thay thế
A supplier should be able to explain not only what work it can perform, but how it determines that the finished tooling remains fit for service.
Before sending tooling for refurbishment, ask:
- How is the initial condition documented?
- Which dimensions are measured before work begins?
- Which defects are accepted for repair?
- Which defects trigger rejection?
- How much material may be removed?
- Can the existing coating be identified and removed safely?
- How is the substrate inspected after coating removal?
- Which dimensions are rechecked after repair or recoating?
- How is tooling-set consistency evaluated?
- What records accompany the completed tooling?
- What happens if the component fails final inspection?
- How are individual tools identified and traced?
- Can the supplier produce replacement tooling from the approved drawing or sample?
Do not assume that a new-tool manufacturer also provides used-tool repair or recoating. Those capabilities require separate confirmation.
When replacement is the technically correct decision, SunshinePro giới thiệu dụng cụ ép máy tính bảng for punches and dies, including standard and non-standard sizes and custom processing from drawings or samples. Trang sản phẩm của họ cũng liệt kê thép tốc độ cao, Gia công CNC, xử lý nhiệt, material inspection reports, and an inspection-and-delivery workflow for new tooling.
Provide the approved drawing, Mẫu, tooling format, material requirement, and inspection expectations when requesting a capability review. For a replacement-tooling discussion, use SunshinePro’s Trang liên hệ rather than assuming that a damaged component can be refurbished.
Chia sẻ:



Được viết bởi Sunshine
Tại Sunshine, Chúng tôi là nhà sản xuất và cung cấp chuyên nghiệp các linh kiện khuôn chính xác, cung cấp một loạt sản phẩm đa dạng cho ứng dụng dập và khuôn ép. Trọng tâm chính của chúng tôi bao gồm khuôn đục lỗ, ghim và ống lót đẩy, và cọc hướng dẫn cùng các bushing. Với gia công CNC tiên tiến, Kiểm soát chất lượng nghiêm ngặt, và năng lực sản xuất mạnh mẽ, chúng tôi đảm bảo độ tin cậy, các bộ phận chính xác cao, cùng với các linh kiện tiêu chuẩn có sẵn trong kho để cung cấp nhanh chóng và hiệu quả toàn cầu.
TIN TỨC
NHẬN DỊCH VỤ
Với các bộ phận chất lượng đáp ứng mọi ngân sách và đội ngũ nhân viên thân thiện được đào tạo để giúp chuyến thăm của bạn trở nên hữu ích và thuận tiện.
