



Kiểm tra độ dài làm việc của máy tính bảng cho máy tính bảng nhất quán
Tablet punch working length is the distance from the punch head flat to the lowest consistently measurable point in the punch cup. A valid inspection measures that distance directly, records every punch individually, and evaluates upper and lower punches as separate sets.
Working-length inspection can help control punch position and reduce one source of tablet thickness, độ cứng, fill, and weight variation. It does not guarantee consistent tablets by itself. Hành vi công thức, hiệu suất cấp liệu, compression settings, điều kiện báo chí, and other tooling dimensions also affect the finished product.
For broader information about punches, cái này, and compatible tooling systems, Xem Các loại dụng cụ ép viên. This guide focuses only on measuring and interpreting punch working length.
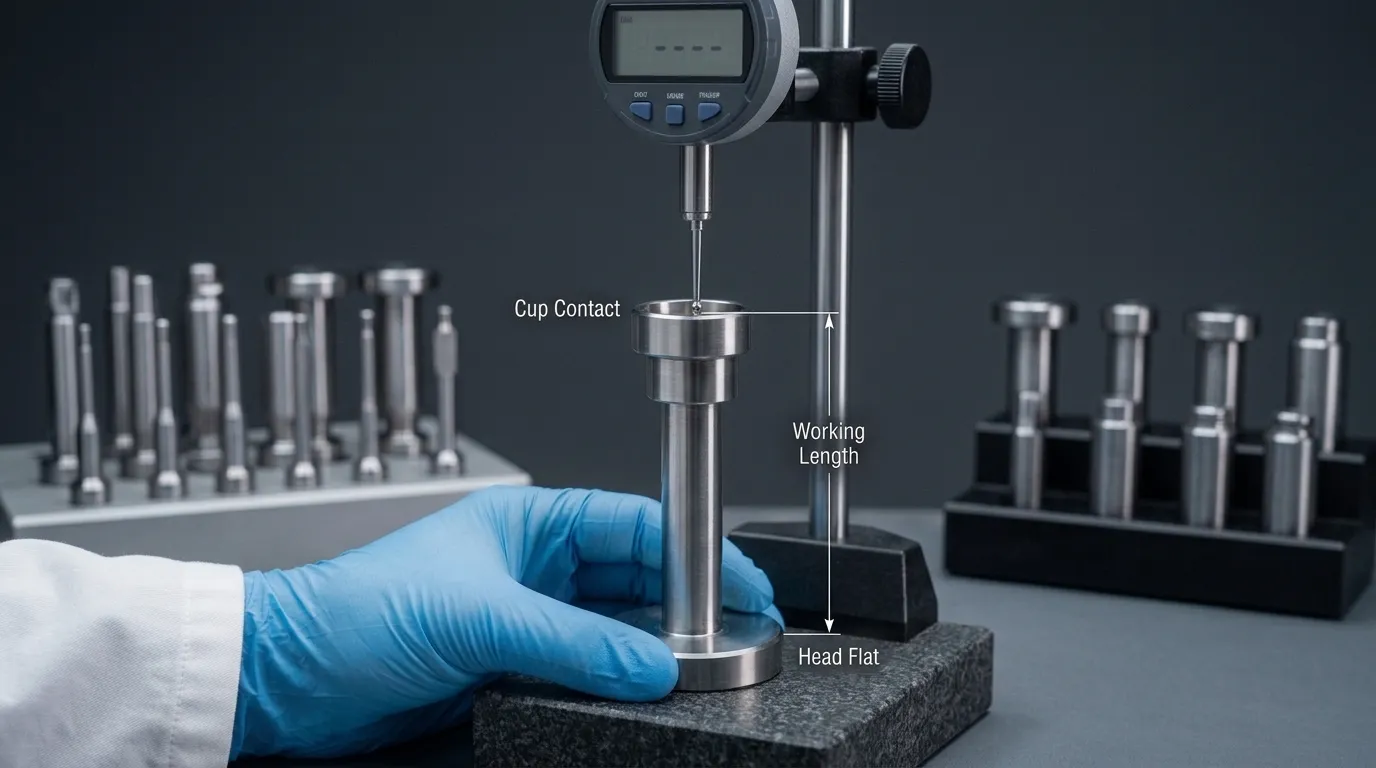
Độ dài làm việc của Punch đo lường gì — và tại sao nó lại quan trọng
A tablet punch has several dimensions, but working length is defined by two specific locations:
- The flat surface on the punch head.
- The lowest repeatable measurement point inside the punch cup.
The word “repeatable” matters. On a plain concave cup, the lowest point may be easy to contact. On an embossed, bisected, or deeply concave punch face, the measuring probe must reach the same defined location on every punch.
Working-length variation changes where individual punches operate relative to the compression rollers and die table. Theo Thảo luận kỹ thuật của Natoli về chiều dài cú đấm và độ sâu cốc, differences within an upper-punch set can contribute to inconsistent compression conditions and variations in tablet thickness or hardness.
Lower-punch working length also affects the punch position inside the die during filling. A shorter or longer lower punch may alter the available fill volume. That can contribute to tablet-weight variation, although powder flow, feeder adjustment, and press settings remain important factors.
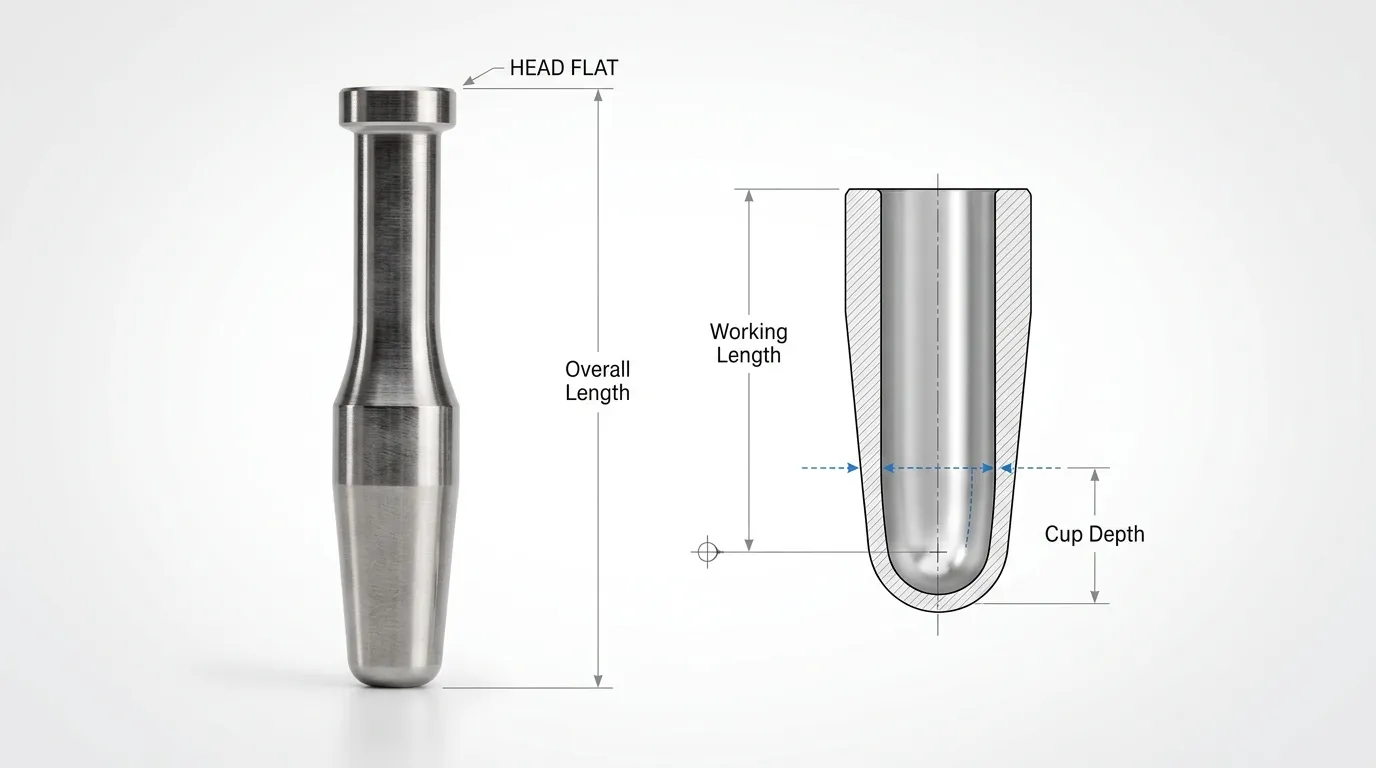
Chiều dài làm việc so với chiều dài tổng thể và độ sâu cốc
These three measurements are related but not interchangeable.
| Kích thước | Điểm đo lường | Mức độ liên quan chính |
|---|---|---|
| Chiều dài làm việc | Ngửa đầu đến điểm thấp nhất có thể đo được nhất quán trong cốc | Vị trí đục lỗ hiệu quả trong quá trình chiết rót và nén |
| Chiều dài tổng thể | Bề mặt đầu đến đầu vật lý xa nhất của đầu đục lỗ | Kích thước và tình trạng kích thước chung của cú đấm |
| Độ sâu cốc | Mặt đầu hoặc mặt đất tham chiếu đến điểm sâu nhất của cốc | Tablet shape, Âm lượng, and cup geometry |
Working length should normally be measured directly. Calculating it by subtracting cup depth from another dimension can combine the errors of two separate measurements. Direct measurement avoids that compounded error when the cup geometry allows reliable probe access.
Thiết lập thông số kỹ thuật quản lý trước khi đo
Do not begin by choosing a tolerance from an article, catalogue, or general industry reference. First identify the document that controls the actual punch set.
The inspection basis should normally follow this order:
- Approved tooling drawing and revision.
- Contractual or purchase specification.
- Approved supplier documentation.
- Internal inspection procedure.
- General industry guidance, used only when it does not conflict with controlled requirements.
Determine whether the inspection must evaluate:
- Each punch against a nominal working length.
- Variation between punches in the same set.
- Both absolute conformance and within-set consistency.
These are separate checks. A group of punches may be closely matched to one another but still fall outside the approved nominal dimension. Ngược lại, every punch may fall within its individual tolerance while the difference between the shortest and longest punch is too large for the approved matching requirement.
Tiêu chuẩn ISO 18084:2011 provides an international framework covering tablet punch-and-die dimensions, các mức dung sai, Đặc điểm, and interchangeability. Its existence does not mean every tooling set has the same working-length acceptance limit, and compliance should not be assumed unless it is stated in the applicable documentation.
Chuẩn bị bộ đục lỗ và hệ thống đo lường
A small measurement difference is meaningful only when the measuring system can detect it consistently. Preparation should address the punches, the fixture, the instrument, and the inspection record.
Before taking readings:
- Separate upper punches from lower punches.
- Confirm the identity or set number of every punch.
- Clean the head flat and the cup contact area.
- Check for residue, các gờ, thiệt hại, or raised material.
- Confirm that each punch can sit in the fixture without rocking.
- Select a probe that can reach the defined cup location.
- Check the indicator’s calibration status.
- Perform any required pre-use reference or zero verification.
- Confirm that the approved drawing and inspection procedure are available.
The indicator should be mounted on a rigid stand or comparable stable fixture. Movement in the base, post, probe, or punch support can appear as dimensional variation even when the punches are identical.
Calibration and verification should follow the site’s documented quality system. Thuộc tính Hướng dẫn xác nhận của Tổ chức Y tế Thế giới calls for inspection instruments to be calibrated and verified under documented programmes, with defined limits, intervals, responsibilities, Truy xuất nguồn gốc, kỷ lục, and actions.
Độ phân giải, Độ chính xác, and Repeatability Are Not the Same
A digital display with many decimal places is not automatically suitable for working-length inspection.
| Đặc tính | Những gì nó cho bạn biết |
| Độ phân giải | Mức tăng nhỏ nhất mà thiết bị hiển thị |
| Độ chính xác | Giá trị tham chiếu gần như thế nào |
| Độ lặp lại | Cùng một thiết lập tạo ra cùng một kết quả nhất quán như thế nào |
| Độ không đảm bảo đo lường | Nghi ngờ liên quan đến kết quả được báo cáo |
An instrument may display very small increments while producing unstable or biased readings. The complete system—including the probe, vật cố định, seating method, operator technique, and environment—must be capable relative to the applicable tolerance.
Borderline results require particular care. When the possible measurement uncertainty is large compared with the remaining distance to the acceptance limit, the reading should not be treated as unquestionable evidence.
Cách đo chiều dài làm việc của máy tính bảng
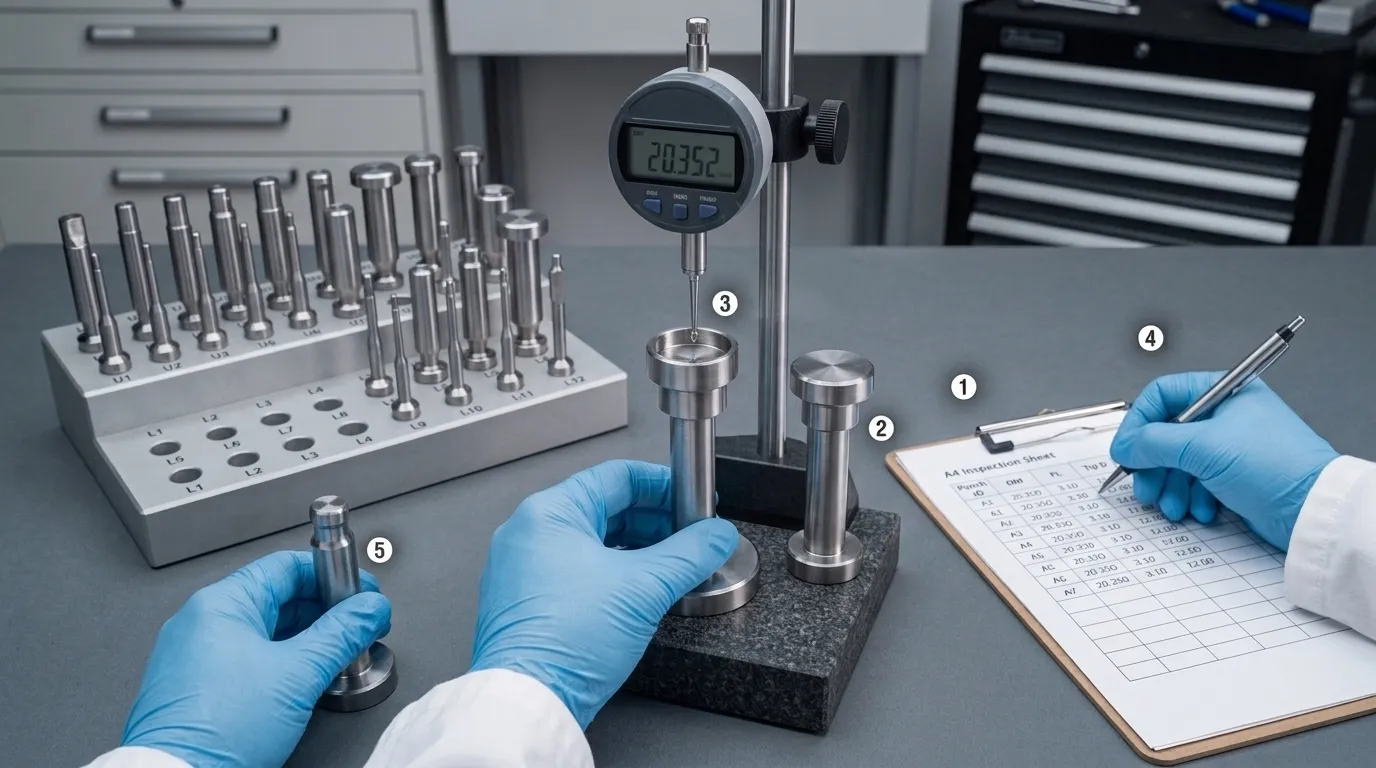
Use the approved site or supplier method where one exists. A typical direct-contact inspection follows this sequence:
- Confirm the reference condition.
Verify the indicator’s zero or reference position using the approved method. - Select the correct punch group.
Measure all upper punches as one dataset. Measure lower punches separately. - Identify the punch.
Record its unique number, set position, or other traceable identifier before taking the reading. - Seat the punch consistently.
Position the head flat against the approved support or datum. The punch must not rock, nghiêng, or sit on residue. - Position the probe.
Bring the contact probe to the defined lowest measurable point in the cup. Use the same location and orientation for every comparable punch. - Apply the approved contact method.
Avoid excessive force. Contact pressure should be consistent and should not damage the punch surface. - Allow the reading to stabilize.
Record the actual displayed result without unnecessary rounding. - Repeat when required.
Remove and reseat the punch if the procedure calls for repeated readings. Repeated measurements help reveal seating or probe-position errors. - Continue through the complete set.
Do not stop after measuring a few apparently similar punches. A single outlier may appear anywhere in the set. - Record abnormalities immediately.
Note unstable readings, difficult probe access, visible wear, damaged surfaces, or any deviation from the approved method.
Do not compare a lower punch with the upper-punch dataset. Their dimensions and functional positions may differ even when they belong to the same tooling set.
Record Each Punch by Identity, Not Just Sequence
A useful inspection record should connect every result to the physical punch. Tối thiểu, kỷ lục:
- Punch identifier.
- Upper or lower designation.
- Tooling set or product reference.
- Số bản vẽ và sửa đổi.
- Instrument identification.
- Calibration or verification status.
- Individual reading.
- Repeated readings, khi cần thiết.
- Final reported result.
- Acceptance criterion.
- Inspector and date.
- Final status or disposition.
Thuộc tính Hướng dẫn GMP của Ủy ban Châu Âu về kiểm soát chất lượng supports maintaining procedures and records for specifications, kiểm tra, calculations, equipment calibration, approval or rejection, and instrument identification.
Tính toán và giải thích kết quả kiểm tra
After measuring the complete upper or lower punch set, identify:
- The minimum working-length reading.
- The maximum working-length reading.
- The difference between them.
Use this calculation:
Phạm vi độ dài làm việc = số đọc tối đa - số đọc tối thiểu
Ví dụ, consider an illustrative upper-punch dataset:
| Cú đấm | Chiều dài làm việc |
| U01 | 133.602 mm |
| U02 | 133.599 mm |
| U03 | 133,604 mm |
| U04 | 133.601 mm |
The minimum is 133.599 mm and the maximum is 133.604 mm.
Range = 133.604 − 133.599 = 0.005 mm
This example demonstrates the calculation only. It does not establish an acceptable limit.
Interpret the data in two stages:
- Compare every punch with the approved nominal dimension and tolerance.
- Compare the set’s maximum-to-minimum range with the approved matching or variation requirement.
A punch set should not be accepted solely because the readings are close together. All punches could be similarly short or similarly long. The nominal dimension and within-set range both need review when the specification requires both.
Why a Common 0.002-Inch Figure Is Not a Universal Limit
Some specialist tooling sources cite a maximum working-length variation of 0.002 inch within a punch set. This figure may be useful as industry context, but it should not automatically be applied to every press, tiêu chuẩn dụng cụ, Sản phẩm, or inspection programme.
The controlling limit must come from the approved drawing, supplier agreement, or internal procedure. The public summary of ISO 18084 does not establish 0.002 inch as a universal working-length acceptance criterion.
Handle Embossed, Bisected, Deep-Cup, and Multi-Tip Punches
Complex punch geometry can make a normal contact measurement unreliable.
| Tính năng đục lỗ | Rủi ro đo lường | Phản ứng thích hợp |
| Dập nổi | Đầu dò tiếp xúc với một ký tự nhô lên thay vì điểm cốc được xác định | Sử dụng một vị trí được chỉ định để tránh tính năng dập nổi |
| Đường hai phần | Đầu dò hạ cánh trên điểm số hoặc ở các phía khác nhau giữa các cú đấm | Xác định hướng và vị trí tiếp xúc nhất quán |
| Cốc lõm sâu | Đầu dò không thể đạt đến điểm thấp nhất mà không có nhiễu | Sử dụng một đầu dò phù hợp hoặc một phương pháp thay thế đã được phê duyệt |
| Cốc không đều | Điểm thấp nhất khó tái tạo | Thiết lập một vật cố định và định hướng được lập thành văn bản |
| Cú đấm đa loại | Một bài đọc tổng thể có thể che giấu sự khác biệt giữa các mẹo | Đánh giá các mẹo riêng lẻ khi thông số kỹ thuật yêu cầu |
Never move the probe to whichever location is easiest on each punch. Changing the contact location can create apparent variation that comes from geometry rather than actual working-length differences.
Where the lowest point cannot be contacted consistently, a different probe, custom fixture, profile-measurement method, or non-contact inspection system may be more appropriate. Thảo luận của Công nghệ Dược phẩm về công nghệ kiểm tra dụng cụ describes the use of data-capture and non-contact systems for more complex or automated inspection tasks.
Xác nhận xem kết quả đọc bất thường có phải là ngoại lệ cú đấm thực sự hay không
One abnormal reading should trigger verification, not an immediate decision to reject or alter the punch.
Sử dụng chuỗi này:
- Recheck the punch identifier.
- Clean the head flat, support surface, and cup contact area.
- Inspect for burrs, dư lượng, thiệt hại, hoặc biến dạng.
- Confirm that the punch is seated correctly.
- Verify the probe location and orientation.
- Recheck the instrument reference.
- Loại bỏ, reseat, and measure the punch again.
- Compare repeated readings.
- Escalate the result if the abnormal value remains stable.
If the repeated values move substantially, the measurement setup may be unstable. If repeated readings remain close to one another but differ from the rest of the set, the punch is more likely to have a real dimensional difference.
Nguyên nhân phổ biến của sự thay đổi thời gian làm việc thực sự
Once measurement error has been ruled out, possible causes include:
- Wear on the punch head flat.
- Uneven or excessive polishing.
- Physical damage or deformation.
- A replacement punch that was not matched to the existing set.
- Upper and lower punches mixed incorrectly.
- Manufacturing or refurbishment variation.
- An incorrect punch from another tooling set.
Không đánh bóng, xay, or otherwise alter a suspected punch before the dimensional condition has been documented and the proper disposition has been approved.
Decide Whether to Accept, Investigate, cách ly, Refurbish, hoặc Thay thế
The confirmed measurement and the governing specification should determine the next action.
| Tìm kiếm | Phản ứng có kiểm soát điển hình |
| Mỗi cú đấm đều đáp ứng các yêu cầu về danh nghĩa và biến thể | Chấp nhận và lập tài liệu |
| Một bài đọc không ổn định hoặc không thể lặp lại | Điều tra thiết lập và đo lường lại |
| Kết quả gần với ranh giới chấp nhận | Xem xét sự không chắc chắn và tuân theo quy trình leo thang đã được phê duyệt |
| Một cú đấm luôn khác với bộ | Quarantine and evaluate matching, sự tân trang, hoặc thay thế |
| Một số cú đấm cho thấy sự rút ngắn dần dần | Investigate wear, điều kiện báo chí, Xử lý, or maintenance practice |
| Bề mặt dữ liệu bị hư hỏng | Cách ly và đánh giá sự phù hợp của việc sửa chữa hoặc thay thế |
| Không thể xác nhận danh tính công cụ | Giữ dụng cụ cho đến khi khả năng truy xuất nguồn gốc được khôi phục |
| Bộ không đáp ứng yêu cầu đã được phê duyệt | Follow the site procedure for rejection, sự tân trang, hoặc thay thế |
Refurbishment is not automatically suitable for every failed punch. Any corrective work can alter critical dimensions and must be followed by appropriate inspection.
Replacement punches should also be evaluated against the existing set rather than treated as acceptable only because they match a nominal catalogue value.
Ghi lại việc kiểm tra và theo dõi sự thay đổi theo thời gian
A one-time result shows the current condition. A series of traceable inspections can reveal how the tooling changes during service.
The inspection record should retain:
- Individual punch readings.
- Phần trên- and lower-set ranges.
- Drawing and revision information.
- Instrument and verification details.
- Any remeasurement activity.
- Visible wear or damage.
- Acceptance decision.
- cách ly, sự tân trang, or replacement action.
Where previous records exist, compare the same punch over time. A gradual reduction in working length may indicate progressive head-flat wear even before the punch exceeds a formal limit.
Trend review should follow approved site rules. Do not create informal warning limits without technical justification, risk assessment, and authorization.
Broader cleaning, Lưu trữ, Xử lý, sự bôi trơn, and inspection-frequency controls belong in a complete Danh sách kiểm tra bảo trì dụng cụ máy tính bảng.
Những gì cần yêu cầu trong báo cáo kết hợp nhà cung cấp
When ordering a replacement punch or a matched tooling set, useful supplier documentation may include:
- Individual punch identification.
- Upper or lower designation.
- Số bản vẽ và sửa đổi.
- Actual working-length readings.
- Measurement method.
- Stated acceptance criterion.
- Instrument or calibration reference, nếu có.
- Matching or grouping information.
- Final inspection status.
Do not assume every supplier provides the same report. Confirm the documentation requirements before placing the order.
Thảo luận về các yêu cầu thay thế hoặc đục lỗ tùy chỉnh với bản vẽ có sẵn
When an inspection confirms a mismatch, damaged punch, or replacement need, prepare the technical information before contacting a supplier:
- Bản vẽ và sửa đổi đã được phê duyệt.
- Tooling type.
- Upper or lower punch designation.
- Existing punch identifiers.
- Individual working-length results.
- Maximum-to-minimum range.
- Description of visible wear or damage.
- Required material or other confirmed drawing requirements.
- Whether one replacement punch or a complete matched set is being considered.
- Hồ sơ kiểm tra bắt buộc.
SunshinePro giới thiệu máy ép viên đục lỗ và khuôn and states that custom tooling can be processed from drawings or samples. The product page also lists high-speed steel and customized size or material options.
For a replacement or custom-tooling enquiry, send the applicable drawing and inspection results through the Trang liên hệ SunshinePro and ask the company to confirm feasibility, measurement documentation, and the specification that would apply to the supplied tooling.
Chia sẻ:



Được viết bởi Sunshine
Tại Sunshine, Chúng tôi là nhà sản xuất và cung cấp chuyên nghiệp các linh kiện khuôn chính xác, cung cấp một loạt sản phẩm đa dạng cho ứng dụng dập và khuôn ép. Trọng tâm chính của chúng tôi bao gồm khuôn đục lỗ, ghim và ống lót đẩy, và cọc hướng dẫn cùng các bushing. Với gia công CNC tiên tiến, Kiểm soát chất lượng nghiêm ngặt, và năng lực sản xuất mạnh mẽ, chúng tôi đảm bảo độ tin cậy, các bộ phận chính xác cao, cùng với các linh kiện tiêu chuẩn có sẵn trong kho để cung cấp nhanh chóng và hiệu quả toàn cầu.
TIN TỨC
NHẬN DỊCH VỤ
Với các bộ phận chất lượng đáp ứng mọi ngân sách và đội ngũ nhân viên thân thiện được đào tạo để giúp chuyến thăm của bạn trở nên hữu ích và thuận tiện.
