



Thiết kế chiều sâu cốc đục viên: Hình dạng, Lực lượng, và Rủi ro Lỗi
Tablet punch cup depth helps determine the finished tablet’s face curvature, central band, and overall appearance. A deeper cup can create a more convex tablet, but it may also reduce punch-tip strength and increase sensitivity to capping, uneven density, or wear under certain operating conditions.
There is no universal best cup depth. The correct design depends on cup radius, đường kính viên, land geometry, required compression load, formulation behavior, và điều kiện báo chí. Cup depth should therefore be evaluated as one part of the wider system of Các loại dụng cụ ép viên, not as an isolated dimension.
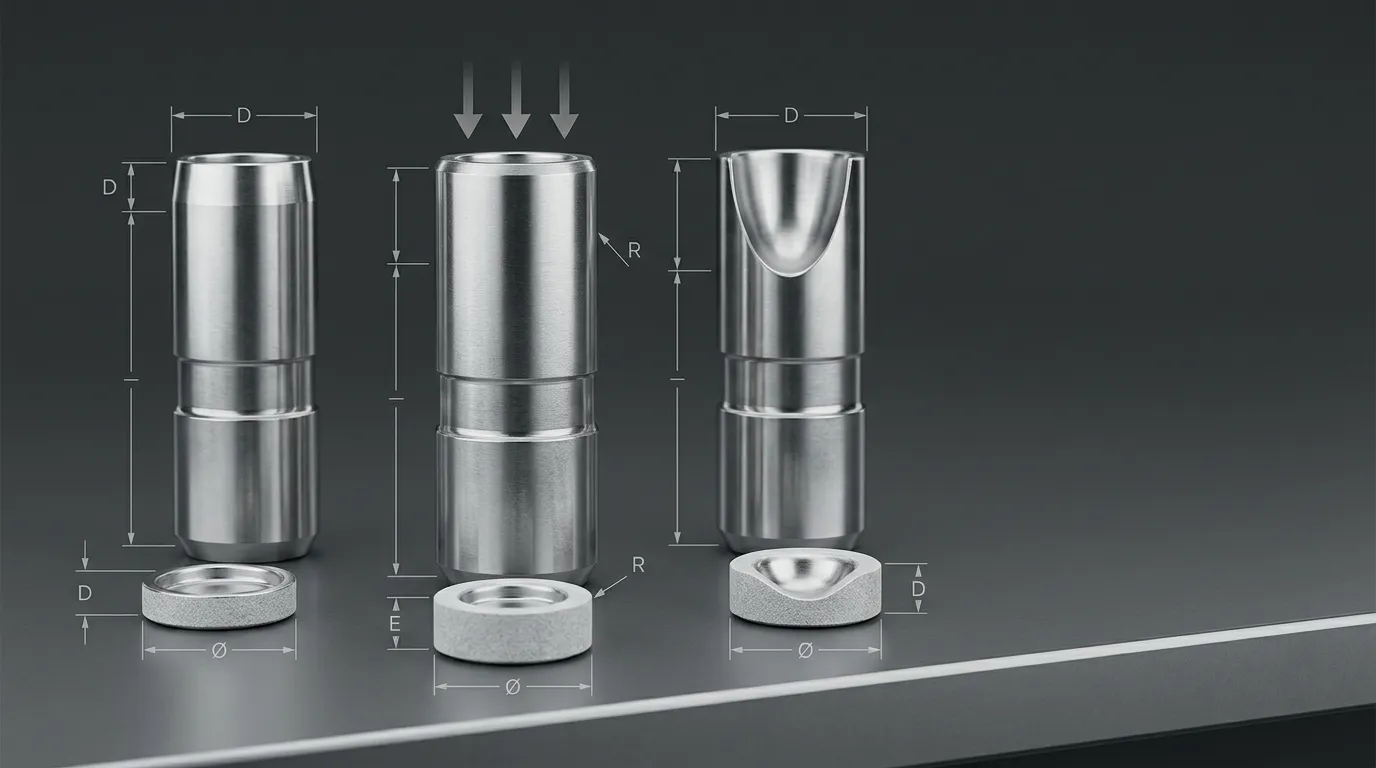
Độ sâu của Tablet Punch Cup đo lường
The punch cup is the recessed area at the end of the punch tip. During compression, the upper and lower cups form the two main faces of the tablet while the die bore forms its central band or sidewall.
Cup depth is the vertical distance from the highest reference surface of the punch tip to the lowest point of the cup. Identification features such as embossed or debossed letters should not be included in this measurement. This distinction follows the terminology used in the Hướng dẫn sử dụng thông số kỹ thuật máy tính bảng APhA.
Cup depth is also separate from punch working length. Working length influences compression position and tablet consistency, while cup depth defines the shape of the tablet face.
Cup Depth, Cup Radius, and Cup Volume Are Different Variables
Cup depth alone does not fully describe the punch profile.
| Biến | Nó mô tả gì | Tại sao điều này lại quan trọng |
|---|---|---|
| Độ sâu cốc | Khoảng cách thẳng đứng từ bề mặt tham chiếu đến điểm thấp nhất của cốc | Influences face height, tablet convexity, and remaining punch-tip section |
| Bán kính cốc | Độ cong được sử dụng để tạo thành cốc | Xác định độ cong của khuôn mặt dần dần hoặc sắc nét |
| Thể tích cốc | Khối lượng chứa trong hồ sơ lõm | Ảnh hưởng đến cách phân bổ thể tích viên nén giữa các mặt và dải trung tâm |
| Tỷ lệ R / D | Bán kính cốc chia cho đường kính viên nén | Giúp so sánh độ cong giữa các viên nén có kích thước khác nhau |
Two punches can have similar cup depths but different radii. One may use a smooth, broad curve, while another reaches the same depth through a steeper profile. Their tablet appearance, stress distribution, and punch-tip strength may therefore differ.
Compound cups make this distinction even more important. Instead of using one continuous radius, a compound profile combines two or more radii. This can create a smooth-looking tablet face while still producing a steep transition near the outer edge.
Cách cốc trên và cốc dưới tạo thành dải máy tính bảng và tổng độ dày
The finished tablet consists of three connected geometric regions:
- the upper cup-formed face;
- the lower cup-formed face;
- the central band formed inside the die.
For a given total tablet thickness, increasing the combined depth of the upper and lower faces generally leaves less thickness in the central band. A narrower band changes the tablet’s proportions and may influence die-wall contact, hành vi đẩy ra, and mechanical failure patterns.
Tablet diameter must also be considered. A 1 mm cup depth does not represent the same curvature on a small tablet and a large tablet. Đường kính, bán kính, Độ sâu, and band thickness must be reviewed together.
Upper and lower cup profiles do not always have to match. A tablet may use symmetrical faces, or one side may be flatter to support branding, Xử lý, Lớp phủ, Bao bì, or application requirements. Any asymmetrical design should still be evaluated as one complete tablet geometry.
So sánh các cấu hình Punch Cup phổ biến như thế nào
The names used for cup profiles describe general forms rather than one universal set of dimensions. A “deep concave” profile from one tooling system or supplier may not have exactly the same depth or radius as another.
| Hồ sơ cốc | Hình dạng chung | Lợi ích thiết kế chính | Hạn chế hoặc rủi ro chính |
| Mặt phẳng | Bề mặt máy tính bảng phẳng | Hình học đơn giản và tải tương đối trực tiếp | Có thể không cung cấp hình thức hoặc đặc điểm xử lý cần thiết |
| Flat-faced bevel edge, or FFBE | Tâm phẳng với cạnh góc cạnh | Xác định cạnh máy tính bảng và có thể giảm góc sắc nét | Hình học vát ảnh hưởng đến phần đầu ngoài và cạnh máy tính bảng |
| Flat-faced radius edge, or FFRE | Trung tâm phẳng với cạnh tròn | Cung cấp chuyển đổi cạnh mượt mà hơn | Chi tiết bán kính vẫn ảnh hưởng đến ứng suất và hành vi nhỏ gọn |
| Lõm nông | Mặt viên nén hơi lồi | Cung cấp độ cong trong khi vẫn duy trì một dải trung tâm tương đối đáng kể | Có thể không đáp ứng yêu cầu về ngoại hình lồi mạnh |
| Lõm tiêu chuẩn | Độ cong khuôn mặt vừa phải | Cân bằng hình thức và tính thực tế của dụng cụ chung | "Tiêu chuẩn" không đại diện cho một chiều phổ quát |
| Lõm sâu | Mặt lồi mạnh | Tạo cấu hình máy tính bảng rõ rệt hơn | Có thể giảm khả năng lực của đầu đục lỗ và tăng độ nhạy với việc đóng nắp |
| Lõm cực sâu | Mặt lồi cao | Hỗ trợ hình dạng viên nén tròn đặc biệt | Tạo ra hình học tích cực hơn và yêu cầu xem xét lực và công thức cẩn thận |
| Cốc hỗn hợp | Khuôn mặt được tạo từ nhiều bán kính | Cho phép kiểm soát nhiều hơn hình thức và hình dạng cạnh | Chỉ riêng độ sâu không thể mô tả tác động của căng thẳng hoặc sức mạnh của nó |
A profile should not be selected solely from this classification. The actual drawing must specify the relevant depth, radius or radii, đất đai, edge transition, đường kính viên, and total thickness.
Tại sao hình dạng cốc sâu hơn có thể làm giảm khả năng lực đục lỗ
The tablet press may be capable of applying a high compression force, but that does not mean every punch-tip design can safely carry that load.
A deeper or steeper cup removes more material from the punch-tip region and changes the path through which compression load passes. The allowable force can depend on:
- tip diameter and shape;
- cup depth and radius;
- single-radius or compound geometry;
- land width and transition geometry;
- punch material and heat treatment;
- existing wear or damage;
- the safety margin applied by the tooling designer.
Specialist tooling guidance consistently warns that machine capacity and punch-tip capacity are separate limits. A tooling design should therefore receive a drawing-specific force assessment rather than relying only on a generic press rating or tooling class.
SunshinePro liệt kê Thép tốc độ cao cao cấp cho dụng cụ ép máy tính bảng. Material is one contributor to strength, but it does not replace a geometry-specific review of the punch tip.
Chuyển đổi từ đất liền và cốc đến cạnh ảnh hưởng như thế nào đến độ bền của đầu mút
The land is the narrow flat area around the perimeter of the punch tip. It provides support at the edge of the cup and influences wear, nhấp nháy, and tablet-band appearance.
A wider or better-supported land may improve edge strength, but changing it can also alter the tablet profile. The transition between the cup and land matters as well. A smooth blend radius generally creates a less abrupt geometric change than a sharp corner.
These details cannot be selected independently:
- Cup depth affects how much material remains beneath the recessed face.
- Land width affects edge support.
- The blend radius affects the transition between the cup and land.
- Tablet appearance limits how much these features can be changed.
There is no universal minimum land width. The correct value depends on the punch shape, Vật chất, compression requirement, tablet appearance, và tiêu chuẩn dụng cụ.
Compression Force, Pressure, Breaking Force, and Tensile Strength
Several different measurements are used in tablet design, and they should not be treated as synonyms.
| Thuật ngữ | Ý nghĩa |
| Lực nén | The load applied by the tablet press, commonly expressed in kilonewtons |
| Áp suất nén | Force divided by an applicable area, commonly expressed in megapascals |
| Lực phá vỡ máy tính bảng | Lực đo được cần thiết để phá vỡ một viên nén thành phẩm trong một thử nghiệm xác định |
| Độ bền kéo | Một thước đo được điều chỉnh theo hình học được sử dụng để so sánh độ bền cơ học của máy tính bảng |
Compression pressure is often used in research because the same force produces different pressure conditions on tablets with different face areas.
Breaking force is a direct test result. Tensile strength attempts to account for tablet dimensions and geometry, making it more useful for some comparisons. Highly convex or unusual profiles may require an equation appropriate to that geometry rather than a formula developed for a flat cylindrical tablet.
Độ sâu của cốc ảnh hưởng như thế nào đến cơ học máy tính bảng và nguy cơ lỗi
During compression, powder does not densify uniformly in every region of a tablet. Punch shape affects how material moves, how pressure is transmitted, and where density or stress gradients develop.
Finite-element and experimental studies have found that convex punch profiles can produce more heterogeneous density distributions than flat punches. Reduced curvature radius and changes in tablet thickness may increase those gradients under the conditions studied. The effect is important because regions with different density or residual stress may respond differently during decompression and ejection.
These findings are directional, not universal. The actual result also depends on formulation properties, compression pressure, Tốc độ, sự bôi trơn, xả khí, đường kính viên, and band thickness.
Tại sao không thể dự đoán rủi ro giới hạn chỉ từ độ sâu
Capping occurs when part of the upper or lower crown separates from the tablet body. Research published in Nghiên cứu dược phẩm found that increasing punch cup depth was associated with a higher capping index in the studied acetaminophen formulation and compression conditions.
Một nghiên cứu riêng biệt trong Tạp chí Dược phẩm Quốc tế showed that tablet diameter, band thickness, curvature ratio, and their interactions influenced capping behavior. Greater curvature, a thinner band, and larger diameter increased capping susceptibility in that experimental system.
These studies do not prove that every deep cup will cap. They show that geometry can increase risk when combined with particular material and process conditions.
Cup-depth assessment should therefore include:
- đường kính viên;
- upper and lower curvature;
- central band thickness;
- formulation compactibility;
- phục hồi đàn hồi;
- target compression pressure;
- press speed and air-release conditions;
- existing capping history.
A shallower cup may reduce one geometric risk while failing to meet appearance, Lớp phủ, Xử lý, or dosage-form requirements. The design decision is a trade-off, not a simple ranking.
Distinguishing Capping, Cán màng, Air Entrapment, and Tool Wear
Not every separation defect is caused by the cup profile.
| Quan sát | Nguyên nhân có thể liên quan đến hình học | Nguyên nhân có thể khác | Những gì cần xác minh |
| Vương miện tách khỏi máy tính bảng | Aggressive curvature, thin band, tập trung ứng suất | Phục hồi đàn hồi, entrapped air, unsuitable pressure or speed | Vị trí thất bại, cup profile, formulation response, điều kiện báo chí |
| Máy tính bảng tách qua một mặt phẳng bên trong | Mật độ hoặc phân bố ứng suất không đồng đều | Bôi trơn, formulation weakness, air pressure | Fracture plane, density pattern, material and process history |
| Chất liệu mỏng xuất hiện xung quanh dây đeo máy tính bảng | Damaged or worn land, clearance issue | Die wear, sự căn chỉnh, lực lượng quá mức | Punch edge, land condition, The Bore, sự căn chỉnh |
| Các khuyết tật tăng lên sau khi sử dụng công cụ kéo dài | Hình dạng cốc hoặc đất hiệu quả đã thay đổi | Trôi quá trình hoặc biến đổi công thức | So sánh các dụng cụ bị mòn với hồ sơ kiểm tra ban đầu |
| Hư hỏng cục bộ xuất hiện gần cạnh máy tính bảng | J-hooking hoặc cạnh đục lỗ bị hỏng | Vấn đề xử lý hoặc đẩy | Hành vi kiểm tra và đẩy đầu tip phóng đại |
Entrapped air is one important non-geometric factor. Research in the Tạp chí Khoa học Dược phẩm shows that internal air pressure can rise during compression and contribute to cracking or capping. Powder permeability, compression speed, tablet size, and consolidation behavior all affect this mechanism.
Cách chọn độ sâu cốc cho máy tính bảng mới hoặc sửa đổi
A useful selection process begins with the required tablet, not with a preferred punch profile.
- Define the finished tablet shape and dimensional limits.
- Select depth and radius together.
- Review the remaining band and edge geometry.
- Estimate the required production compression conditions.
- Confirm the allowable force for the proposed punch tip.
- Review formulation and process sensitivity.
- Compare less aggressive alternatives.
- Validate the final design through compression trials and inspection.
Bắt đầu với hình dạng và dây đeo máy tính bảng cần thiết
Document the dimensions and functional requirements before choosing the cup profile:
- tablet diameter or major and minor axes;
- target total thickness;
- required band thickness;
- upper and lower face shape;
- edge style;
- coating and handling requirements;
- branding or identification area;
- packaging and feeding constraints.
The design team should then determine whether the appearance can be produced with a broader radius or shallower depth. A small geometric change may preserve the visual profile while increasing punch-force margin or reducing capping sensitivity.
Upper and lower profiles should also be assessed separately. A symmetrical tablet may be visually desirable, while an asymmetrical tablet may provide a flatter identification surface or better handling characteristics.
Kiểm tra công thức và độ nhạy của quy trình
The same cup geometry can behave differently with two formulations. Relevant material properties include:
- compactibility;
- plastic or brittle deformation behavior;
- phục hồi đàn hồi;
- permeability;
- lubricant sensitivity;
- moisture condition;
- previous capping or lamination history.
Press conditions matter as well. Precompression may assist air release and early consolidation, while press speed affects the time available for densification and decompression. Detailed consolidation-time decisions belong to đầu đục lỗ máy tính bảng phẳng và thời gian dừng, but cup depth should still be reviewed alongside those conditions.
Geometry cannot automatically compensate for a formulation that does not form a stable compact. It also should not be changed before confirming that the defect is not being caused by air entrapment, sự bôi trơn, Áp lực, Tốc độ, sự căn chỉnh, or worn tooling.
Xác nhận biên độ lực dụng cụ và xác nhận thiết kế cuối cùng
Before manufacturing the full tooling set, xác nhận:
- the press and tooling standard;
- the proposed upper and lower cup drawings;
- the material and heat-treatment specification;
- the expected operating-force range;
- the allowable punch-tip force for the proposed geometry;
- the required safety margin;
- the cup, đất đai, bán kính, and working-length tolerances;
- the trial and acceptance criteria.
Production trials should use the actual formulation, intended press, realistic operating speed, and expected pressure range. Evaluation should include tablet dimensions, Ngoại hình, breaking behavior, nắp, cán màng, sự đẩy ra, và tình trạng đục lỗ.
A profile is ready for approval only when both sides of the design are acceptable: the punch can withstand the operating conditions, and the formulation can produce a stable tablet with the required shape.
Những gì cần chỉ định trên bản vẽ đục lỗ và RFQ
A tooling supplier cannot assess cup depth from a tablet image alone. The RFQ should separate the required tablet geometry from the tooling, báo chí, và điều kiện sản xuất.
SunshinePro states that custom tablet tooling can be processed from drawings or samples and that its workflow includes drawing submission, đánh giá thiết kế, Báo giá, Sản xuất, Kiểm tra, and delivery. A controlled drawing remains the clearest way to define the required geometry.
Hình học và thông tin ứng dụng cần bao gồm
| Thông tin | Tại sao điều này lại quan trọng |
| Đường kính máy tính bảng hoặc trục chính và trục phụ | Thiết lập tỷ lệ của hình học khuôn mặt |
| Tổng độ dày mục tiêu | Xác định hồ sơ hoàn chỉnh |
| Độ dày dải yêu cầu | Kiểm soát thành bên trung tâm và vùng tiếp xúc khuôn |
| Độ sâu cốc trên và dưới | Xác định từng khuôn mặt độc lập |
| Bán kính cốc hoặc bán kính hợp chất | Mô tả độ cong chứ không chỉ chiều sâu |
| Chiều rộng đất | Xác định hỗ trợ đục lỗ và cạnh máy tính bảng |
| Bán kính pha trộn hoặc chuyển tiếp | Kiểm soát quá trình chuyển đổi từ cốc sang đất |
| Kiểu cạnh | Ảnh hưởng đến cạnh máy tính bảng và hình dạng đục lỗ |
| Dập nổi hoặc dập nổi | Thay đổi hình học cục bộ và các tính năng nhận dạng |
| Máy ép viên và tiêu chuẩn dụng cụ | Xác nhận khả năng tương thích vật lý |
| Lực dự kiến hoặc phạm vi áp suất | Hỗ trợ đánh giá độ bền của dụng cụ |
| Công thức và lịch sử lỗi đã biết | Xác định rủi ro cụ thể của ứng dụng |
| Yêu cầu về bề mặt và kiểm tra | Thiết lập tiêu chí chấp nhận |
A supplier should also know whether an existing tablet or punch sample is being reproduced. A sample may help communicate shape, but it should not replace a controlled drawing when exact depth, bán kính, đất đai, and tolerance matter.
Khoan dung, Kiểm tra, and Documentation Requirements
Feature-specific tolerances should be agreed on the drawing. A general supplier capability does not prove that every cup feature can or should use the same tolerance.
Define how the following will be checked:
- upper and lower cup depth;
- cup radius or profile;
- land width;
- tip dimensions;
- chiều dài làm việc;
- chiều dài tổng thể;
- consistency across the punch set;
- material identification;
- final inspection records.
SunshinePro’s tablet tooling page publishes a general tolerance capability of ±0.002 mm and states that material inspection reports can be provided. That figure should still be confirmed against the actual cup feature, drawing geometry, inspection method, and production requirement.
Nó đã nêu Phương pháp kiểm soát chất lượng includes raw-material inspection, giám sát trong quá trình, kiểm tra cuối cùng, and inspection reporting. Buyers should specify which records are required for the particular tooling order.
Làm thế nào mài mòn có thể thay đổi độ sâu cốc hiệu quả và nguy cơ khuyết tật
An approved cup design can change during production life.
Repeated polishing may gradually reduce effective cup depth, alter the radius, narrow the land, or round the edge transition. Uneven wear across a punch set can also produce differences in tablet thickness or face shape.
Common wear-related warning signs include:
| Triệu chứng sản xuất | Kiểm tra dụng cụ |
| Mặt máy tính bảng trở nên ít rõ ràng hơn | So sánh độ sâu và cấu hình cốc với bản vẽ đã được phê duyệt |
| Thay đổi giao diện của dây đeo máy tính bảng | Inspect land width, edge transition, and die condition |
| Đóng nắp xuất hiện sau một thời gian sản xuất ổn định | Check for J-hooking, worn land, altered cup geometry, and process drift |
| Kích thước khác nhau tùy theo trạm | So sánh các cú đấm trên toàn bộ |
| Nhấp nháy xuất hiện xung quanh dây đeo | Inspect punch-tip edges, Cuộc Thanh Tra, mặc, và sự căn chỉnh |
J-hooking occurs when the punch-tip edge becomes deformed or develops a hooked profile. This damaged edge may disturb tablet release and contribute to capping, cán màng, or flashing.
Before redesigning the cup, compare the current tooling with its original measurement and inspection records. A design that performed correctly when new may be experiencing a maintenance or wear problem rather than a fundamental geometry error.
Những sai lầm thường gặp trong thiết kế độ sâu cốc
- Chọn độ sâu chỉ từ hình thức máy tính bảng
Appearance does not reveal punch-tip strength, density distribution, or formulation sensitivity. - Xử lý độ sâu và bán kính có thể hoán đổi cho nhau
Two profiles with the same depth can have different curvature and stress behavior. - Bỏ qua đường kính máy tính bảng
A fixed depth has a different meaning on different tablet sizes. - Bỏ qua dải trung tâm
Deeper faces may reduce band thickness and change mechanical behavior. - Sử dụng công suất máy làm giới hạn lực đục lỗ
The press may be able to apply more load than the punch tip can safely withstand. - Không xác định chi tiết đất đai và chuyển tiếp
The cup edge is part of the structural design, not a minor finishing feature. - Giả sử tất cả các cốc sâu đều gây ra nắp
Depth may increase susceptibility, but formulation and process conditions determine the actual result. - Giả sử cốc nông loại bỏ các khuyết tật
Capping and lamination can still result from air, phục hồi đàn hồi, sự bôi trơn, Áp lực, mặc, or other causes. - Sao chép hồ sơ từ đường kính máy tính bảng khác
The depth-to-diameter and radius-to-diameter relationships may be different. - Bỏ qua mài mòn dụng cụ
A worn punch may no longer match the approved cup profile. - Áp dụng dung sai chung cho mọi tính năng
Độ sâu cốc, bán kính, đất đai, and working length may require different controls. - Phê duyệt bản vẽ mà không thử nghiệm liên quan đến sản xuất
Dimensional correctness does not prove formulation compatibility.
Khi nào nên liên quan đến nhà cung cấp dụng cụ máy tính bảng
Supplier review is useful when the cup is deep, compound, asymmetrical, unusually small, intended for high compression load, or associated with recurring tablet defects. It is also appropriate when an existing punch or tablet sample must be reproduced.
SunshinePro của dụng cụ ép máy tính bảng page confirms punches and dies, Thép tốc độ cao cao cấp, standard and non-standard size options, and customization based on drawings or samples. It also states that material inspection reports are available.
Trước khi đặt hàng, request drawing-specific confirmation of:
- upper and lower cup geometry;
- Vật chất;
- feature tolerances;
- press and tooling compatibility;
- inspection method;
- Tài liệu;
- allowable punch-tip force.
SunshinePro does not publicly confirm formulation testing, finite-element analysis, capping trials, or pharmaceutical-process validation. Those requirements should be discussed and verified separately rather than assumed from its general tooling capabilities.
Once the tablet geometry, expected operating conditions, and inspection requirements are defined, Gửi bản vẽ dụng cụ hoặc mẫu for manufacturing review and quotation.
Chia sẻ:



Được viết bởi Sunshine
Tại Sunshine, Chúng tôi là nhà sản xuất và cung cấp chuyên nghiệp các linh kiện khuôn chính xác, cung cấp một loạt sản phẩm đa dạng cho ứng dụng dập và khuôn ép. Trọng tâm chính của chúng tôi bao gồm khuôn đục lỗ, ghim và ống lót đẩy, và cọc hướng dẫn cùng các bushing. Với gia công CNC tiên tiến, Kiểm soát chất lượng nghiêm ngặt, và năng lực sản xuất mạnh mẽ, chúng tôi đảm bảo độ tin cậy, các bộ phận chính xác cao, cùng với các linh kiện tiêu chuẩn có sẵn trong kho để cung cấp nhanh chóng và hiệu quả toàn cầu.
TIN TỨC
NHẬN DỊCH VỤ
Với các bộ phận chất lượng đáp ứng mọi ngân sách và đội ngũ nhân viên thân thiện được đào tạo để giúp chuyến thăm của bạn trở nên hữu ích và thuận tiện.
