



Chốt đục lỗ cho dập thép không gỉ: Tùy chọn vật liệu và lớp phủ
There is no single best material or coating for punch pins used in stainless steel stamping. The right combination depends on the stainless grade and condition, độ dày tấm, hình học đục lỗ, khối lượng sản xuất, sự bôi trơn, die alignment, Giải phóng mặt bằng, and the failure mode already appearing in production.
A punch substrate provides the bulk toughness, độ bền nén, and edge support. Heat treatment establishes its usable hardness and fracture resistance. Surface finish affects friction and material pickup. The coating or surface treatment then modifies wear, Nhiệt, and sliding behavior. Choosing only one of these elements rarely solves the complete problem.
This guide focuses on punch pins used to pierce or blank stainless steel sheet. It does not assume that the punch itself must be made from stainless steel. Để biết thông tin rộng hơn về các loại khuôn, system-level material selection, Giải phóng mặt bằng, các mức dung sai, và nguồn cung, xem Hướng dẫn đục lỗ (được suy luận).
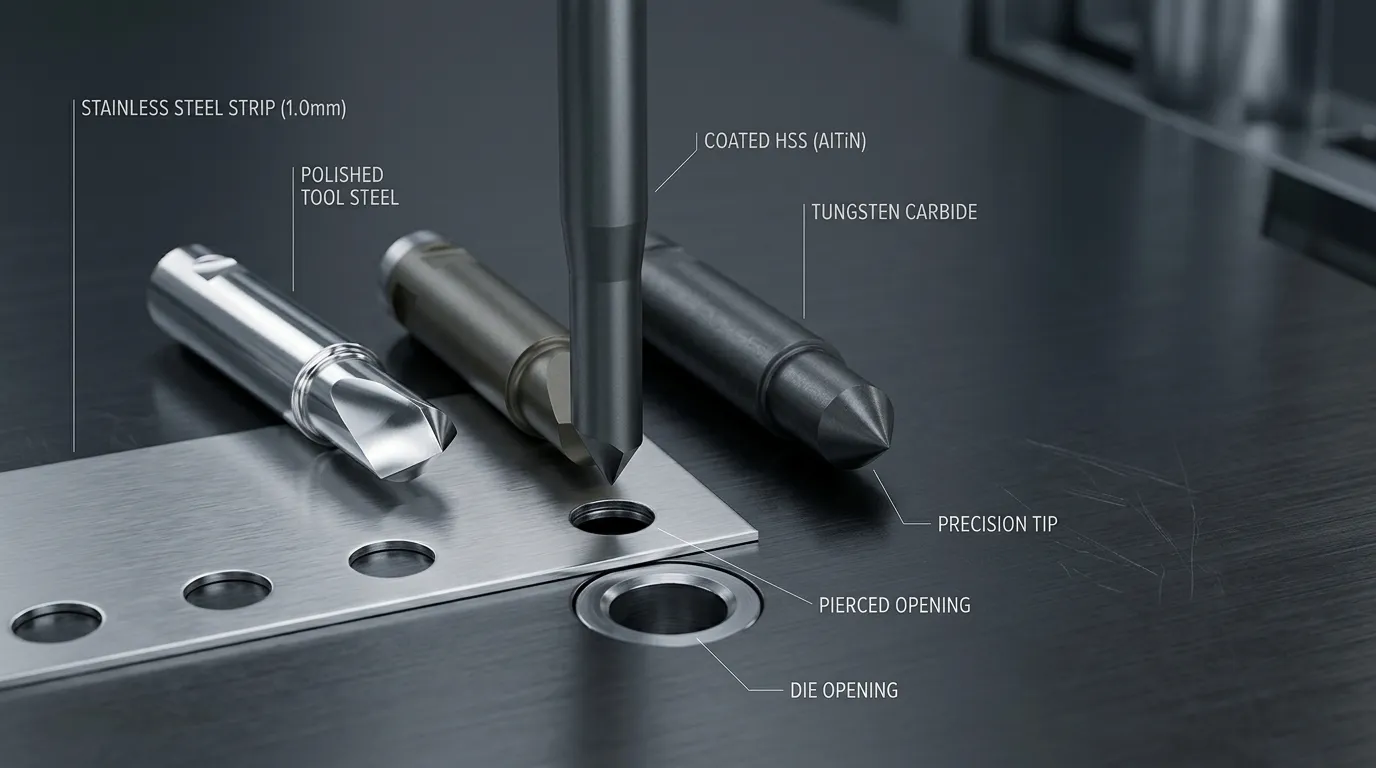
Tại sao thép không gỉ thay đổi lựa chọn chốt đục lỗ
Stainless steel is not one uniform work material. Austenitic, ferritic, martensitic, and duplex grades have different mechanical properties and forming behavior. Thuộc tính WorldStainless Tổng quan về các dòng thép không gỉ is useful background, but the tooling decision must go further than identifying the family name.
The supplier or tool engineer should know:
- the exact stainless grade;
- độ dày tấm;
- temper, độ cứng, or tensile condition;
- điều kiện bề mặt;
- pierced-hole or blank geometry;
- expected production quantity;
- lubrication method or restrictions;
- current punch material and coating;
- the actual failure seen in production.
Stainless applications often create high contact pressure, ma sát trượt, and heat at the punch surface. Under unfavorable conditions, workpiece material can transfer onto the punch. This adhesive wear process is commonly described as galling or material pickup.
Đánh giá ngang hàng về mài mòn trong hình thành kim loại explains that friction, điều kiện bề mặt, Áp lực, Nhiệt độ, and wear development interact during the process. Once pickup begins, the roughened punch surface can attract more material, increase stripping force, damage the sheet surface, and accelerate further wear.
Stainless sheet may also work-harden near the cutting zone. Thicker or stronger material raises the load on the cutting edge. These conditions make it risky to choose a punch only by nominal hardness.
Chọn chất nền đục lỗ trước khi chọn lớp phủ
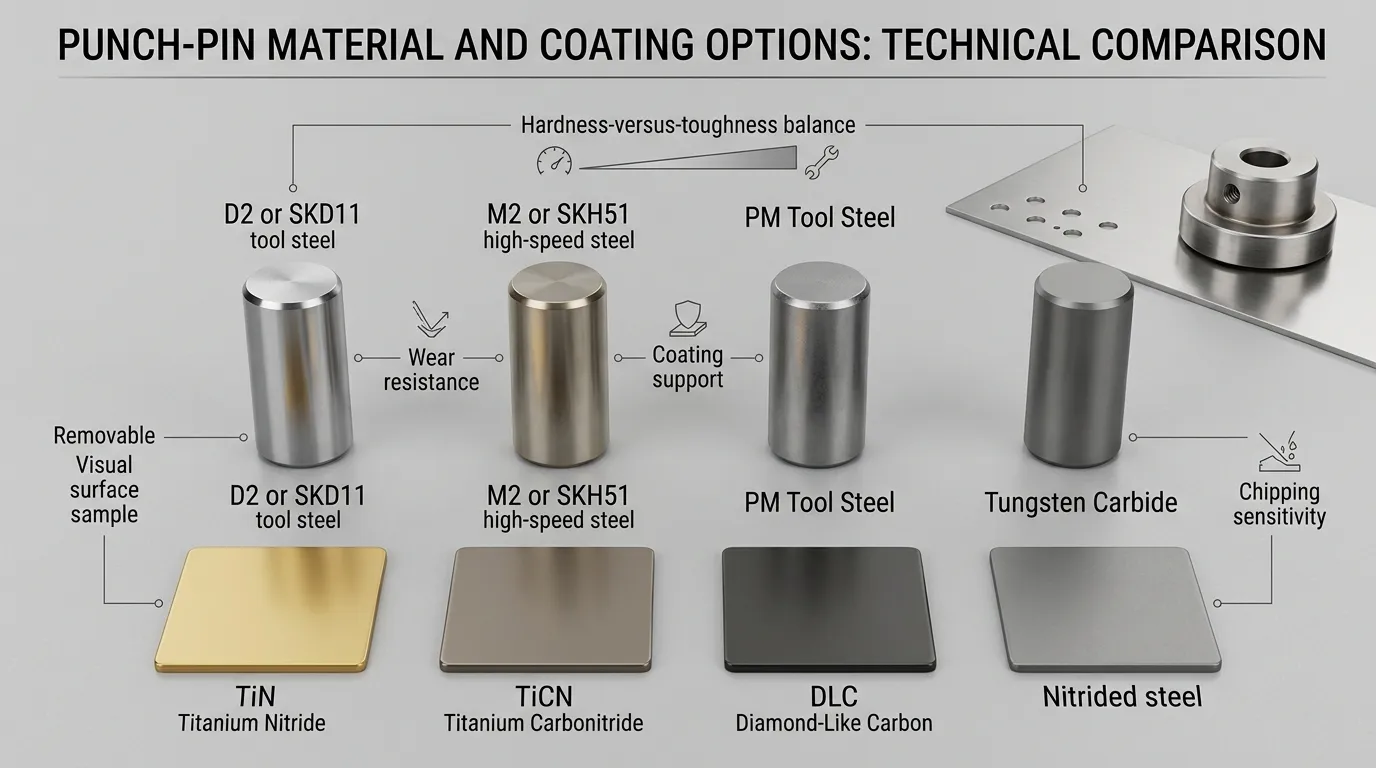
The coating is supported by the material underneath it. A hard coating on an unsuitable, poorly heat-treated, or damaged substrate can still crack, delaminate, chip, or fail with the cutting edge.
The main punch-material options should be compared using several properties:
| Đục lỗ nền | Điểm mạnh chính | Main limitations | Lý do điển hình để xem xét nó |
|---|---|---|---|
| Thép công cụ loại D2 hoặc SKD11 | Chống mài mòn, độ bền nén, độ ổn định kích thước | Can be less tolerant of impact, deflection, or sharp stress concentrations than tougher grades | Hình học ổn định và sản xuất dẫn đầu mài mòn vừa phải |
| M2, SKH51, or SKH9 HSS | Better balance of wear resistance, sự cứng cáp, và khả năng chịu nhiệt | Higher cost than conventional tool steel; still dependent on correct heat treatment | Stainless, thicker sheet, coated punches, or higher production demands |
| Thép công cụ PM | Cân bằng độ bền mài mòn mạnh mẽ và cấu trúc vi mô đồng đều hơn | Chi phí vật liệu cao cấp và các yêu cầu xử lý cụ thể | Khi thép thông thường mòn quá nhanh nhưng cacbua quá giòn |
| Thép công cụ chống va đập | Độ dẻo dai cao và khả năng chống gãy liên quan đến va đập | Khả năng chống mài mòn thấp hơn so với các loại mài mòn hợp kim mạnh | Sứt mẻ hoặc va đập quan trọng hơn mài mòn dần dần |
| Cacbua vonfram | Very high hardness, độ bền nén, và khả năng chống mài mòn | Brittle under misalignment, sốc, deflection, or poor edge support | Sản xuất độ mài mòn cao ổn định với dụng cụ cứng |
| Thép công cụ không gỉ như SUS420 hoặc SUS440 | Chống ăn mòn và đánh bóng | Không tự động là chất nền tốt nhất để xuyên tấm không gỉ | Môi trường ăn mòn hoặc các ứng dụng mà bản thân cú đấm cần chống ăn mòn |
D2 or SKD11 for Stable, Wear-Led Applications
D2-class cold-work tool steel is widely used where wear resistance and compressive strength are important. Material documentation for BÖHLER K110, a D2-class steel, lists stamping and blanking among its applications and emphasizes wear resistance and dimensional stability.
D2 or SKD11 may be a reasonable starting point when:
- the punch has a robust cross-section;
- alignment and clearance are controlled;
- production volume is moderate;
- gradual wear is the main concern;
- sudden chipping or bending is not occurring.
It becomes a weaker choice when the punch is very slender, has sharp corners, experiences side loading, or breaks before the cutting edge wears out. Trong những trường hợp đó, additional hardness may make the problem worse rather than better.
M2, SKH51, or SKH9 When Toughness and Heat Resistance Matter More
High-speed steel is commonly evaluated when the punch needs a stronger balance of wear resistance, sự cứng cáp, and resistance to heat generated during repeated cycling.
Hướng dẫn kỹ thuật từ CONIC trên vật liệu dụng cụ associates M2-type material with stainless steel, thicker sheet, coating use, and larger production quantities. That does not make M2 a universal answer, but it explains why HSS often appears in stainless stamping recommendations.
SunshinePro của Đục lỗ thép tốc độ cao page lists SKH51 and SKH9 among its material options, along with vacuum heat treatment, mài chính xác, EDM, and optional TiN or TiCN coatings. These are company-specific product options, not fixed specifications for every application.
HSS is worth evaluating when:
- D2 wears or chips too quickly;
- surface heat is significant;
- the punch will receive a PVD coating;
- production volume justifies a higher-cost substrate;
- the geometry needs more fracture resistance than conventional wear steel provides.
Thép công cụ PM để cân bằng độ mài mòn – độ dẻo dai cao hơn
Powder-metallurgy tool steels are useful when both wear and fracture resistance matter. Their more uniform microstructure can provide a better combination of properties than many conventionally produced tool steels.
Ví dụ, the manufacturer describes BÖHLER K490 MICROCLEAN as a PM cold-work steel combining wear resistance, độ bền nén, sự cứng cáp, and dimensional stability for applications that include stamping and blanking.
PM steel may be justified when:
- conventional D2-type steel wears too quickly;
- HSS does not provide the required service interval;
- carbide chips under the existing geometry or loading;
- downtime costs more than the material upgrade;
- repeated regrinding and stable dimensional behavior are important.
The recommendation must still be grade-specific. “PM steel” is a manufacturing category, not one standardized set of properties.
Carbide for Stable High-Wear Conditions, Not Every High-Volume Job
Tungsten carbide offers high hardness, độ bền nén, and resistance to abrasive wear. It can be effective in stable, high-volume applications where the punch receives rigid support and loading remains predictable.
Its main limitation is brittleness. Carbide is less forgiving of:
- sai lệch;
- sự lệch cú đấm;
- impact or interrupted loading;
- weak corner geometry;
- hỗ trợ không đầy đủ;
- slug interference;
- tải bên;
- giấy phép không đúng.
A carbide punch that chips after a few cycles is not improved by selecting an even harder carbide grade without correcting the mechanical cause.
SunshinePro của cú đấm cacbua page lists tungsten carbide, mài chính xác, EDM, customized dimensions, and TiN, TiCN, or DLC coating options. Suitability still requires a review of the punch geometry, phôi, điều kiện báo chí, và lịch sử thất bại.
Khi một cú đấm bằng thép không gỉ thực sự là yêu cầu
A punch used on stainless steel does not automatically need a stainless substrate.
Corrosion-resistant grades such as SUS420 or SUS440 may be selected when the tool itself is exposed to moisture, corrosive substances, frequent cleaning, or an environment where rust resistance matters. SunshinePro lists these grades on its separate stainless punch-pin product page.
That is a different engineering requirement from selecting a wear-resistant punch for stainless sheet. In many stamping applications, HSS, PM steel, conventional tool steel, or carbide may provide a more useful balance of wear, sự cứng cáp, and edge stability.
Kết hợp lớp phủ hoặc xử lý bề mặt với chế độ hỏng hóc
Coating choice should begin with the observed surface failure.
- Mòn hoặc mài mòn chất kết dính: prioritize low friction, resistance to material transfer, chuẩn bị bề mặt, và bôi trơn.
- Abrasive wear: prioritize surface hardness and resistance to gradual material loss.
- High heat: review thermal stability and compatibility with the substrate’s heat-treatment condition.
- Chipping or fracture: correct the substrate, hình học, sự căn chỉnh, or loading before focusing on the coating.
- Lực tước cao: inspect pickup, Kết thúc, sự bôi trơn, and punch withdrawal conditions.
A coating name alone is not enough. Performance also depends on coating thickness, độ bám dính, quy trình lắng nghe, edge preparation, substrate hardness, nhiệt độ hoạt động, và hoàn thiện bề mặt.
TiN and TiCN Are Common Options, Not Universal Answers
TiN is one of the most familiar hard coatings used on tooling. It can improve wear resistance in suitable systems, but it should not automatically be described as the preferred stainless-steel coating.
Ví dụ, Hướng dẫn sơn phủ của Dayton Lamina assigns different treatments to adhesive wear, mài mòn, Nhiệt, and specific work materials. Its recommendations also show that TiN is not universally preferred for stainless applications.
TiCN is commonly considered where higher wear resistance and improved sliding behavior are required. It may be evaluated for abrasive wear or material-pickup problems, but its performance still depends on substrate support, chuẩn bị bề mặt, coating quality, và điều kiện vận hành.
SunshinePro lists TiN and TiCN as available options on its HSS and stainless-steel punch-pin pages. The final selection should be based on the actual application rather than coating popularity.
AlTiN hoặc AlCrN cho các điều kiện liên quan đến nhiệt
AlTiN and AlCrN coatings are often considered where elevated surface temperature and demanding wear conditions are central concerns.
Before selecting either coating, xác nhận:
- the substrate’s tempering resistance;
- coating-process temperature;
- required friction behavior;
- edge preparation;
- độ bám dính lớp phủ;
- whether heat or galling is the dominant failure.
A heat-resistant coating will not correct an unsupported edge or a punch that bends under load.
DLC và hệ thống nhiều lớp bôi trơn để mài mòn chất kết dính
DLC and other low-friction multilayer systems may be considered where adhesive wear, gây khó chịu, and high stripping force dominate.
Hướng dẫn kỹ thuật từ các nhà sản xuất dụng cụ như Độ chính xác của Mate connects low-friction coating selection with lubrication restrictions, punch dimensions, độ dày tấm, and deflection. This is important because a lubricious surface can reduce friction, but it cannot stabilize a weak punch geometry.
DLC suitability depends on the substrate, quy trình lắng nghe, service temperature, độ bám dính lớp phủ, và tải trọng cạnh. SunshinePro lists DLC on its carbide-punch page, but that does not confirm availability or suitability for every punch material.
Thấm nitơ khi xử lý khuếch tán phù hợp với kế hoạch dịch vụ
Nitriding hardens the punch surface by diffusion rather than adding a separate deposited layer. It can be useful where surface hardness and geometry coverage are important.
Its selection should consider:
- substrate compatibility;
- case depth;
- hoàn thiện bề mặt yêu cầu;
- thay đổi kích thước;
- hạn mức xay lại;
- whether the treated layer will remain after sharpening.
Nitriding should not be described as a SunshinePro capability unless confirmed for the specific order. It remains a general technical option to discuss with the tooling and treatment supplier.
Chẩn đoán lỗi trước khi nâng cấp công cụ
A more expensive material or coating is useful only when it addresses the actual failure.
| Triệu chứng quan sát được | Cơ chế có thể xảy ra | Kiểm tra trước khi nâng cấp | Hướng vật liệu có thể | Hướng bề mặt có thể |
| Tích tụ không gỉ trên cú đấm | Mài mòn hoặc mài mòn chất kết dính | Kết thúc, sự bôi trơn, Nhiệt, Giải phóng mặt bằng, stripping action | Giữ lại chất nền cứng nếu nó không bị biến dạng hoặc sứt mẻ | Low-friction PVD, DLC-type system, nitride hóa, or improved polishing depending on conditions |
| Làm tròn cạnh dần dần | Abrasive wear | Workpiece condition, Giải phóng mặt bằng, punch hardness, khối lượng sản xuất | HSS, PM steel, or carbide if the process is stable | TiCN hoặc một lớp phủ tập trung vào mài mòn khác |
| Chip nhỏ ở lưỡi cắt | Gãy cục bộ hoặc không đủ độ dẻo dai | Hình học cạnh, sự căn chỉnh, các góc, giá đỡ đục, xử lý nhiệt | Tougher HSS, PM steel, or shock-resistant steel | Không coi lớp phủ là cách khắc phục chính |
| Đấm đột ngột bị gãy | Mechanical overload, deflection, sai lệch, or brittle substrate | Hướng dẫn, tiền dự phòng, Giải phóng mặt bằng, slug interference, punch length | Chất nền dẫn dẻo dai sau khi khắc phục nguyên nhân cơ học | Lớp phủ là thứ cấp |
| Biến dạng cạnh hoặc lật | Inadequate hardness, độ bền nén, hoặc hỗ trợ | Xử lý nhiệt, punch load, Độ dày, hình học | Higher-strength tool steel, HSS, PM steel, or carbide where stable | Chỉ mài mòn lớp phủ sau khi hiệu chỉnh chất nền |
| Lực rút cao | Pickup, poor stripping, lớp hoàn thiện thô, or inadequate lubrication | Stripper condition, punch surface, chất bôi trơn, tải bên | Duy trì đủ độ dẻo dai cho tải rút | Xử lý ma sát thấp khi tương thích |
Chẩn đoán gãy xương tổng quát nằm trong hướng dẫn riêng đục lỗ đứt gãy trong khuôn dập. The critical point here is that chipping and breakage often indicate a bulk-material or mechanical problem, not a missing coating.
Kiểm tra hình dạng và điều kiện khuôn trước khi đổ lỗi cho vật liệu
The punch operates as part of a complete die system. Before changing the substrate or coating, inspect the conditions that control how the load reaches the cutting edge.
- Confirm punch alignment. Misalignment creates uneven edge loading and can chip even a premium punch.
- Review punch-and-die clearance. Clearance should match the workpiece material and thickness. An unsuitable value can increase force, sự hình thành răng cưa, mặc, and fracture risk.
- Inspect the stripper and guide system. Poor guidance or abnormal stripping can bend the punch during withdrawal.
- Check the retainer and mounting condition. Movement at the head or shank changes how the punch is loaded.
- Inspect for slug interference. A trapped or pulled slug can create sudden overload.
- Review the punch surface. Grinding marks, thiệt hại, or pickup can accelerate galling.
- Confirm lubrication. Restricted lubrication changes the friction and coating requirements.
- Account for coating thickness. Final dimensions and tolerances should reflect the complete coated condition.
Thuộc tính Hướng dẫn thành phần khuôn provides broader information about punches, ghim, các vòng đệm, Các thành phần hướng dẫn, and wear parts.
Những cú đấm nhỏ và mảnh mai cần được đánh giá đầu tiên về độ dẻo dai
A small-diameter or high-aspect-ratio punch can deflect before the cutting edge reaches its nominal material limit.
Risk rises when the punch has:
- chiều dài không hỗ trợ quá mức;
- những góc sắc nhọn;
- các đoạn hẹp;
- tải bên;
- interrupted contact;
- hướng dẫn kém;
- heavy stripping force.
In this situation, selecting carbide or maximizing hardness can increase chipping risk. A tougher HSS or PM steel, Chiều dài không hỗ trợ ngắn hơn, stronger guidance, and improved corner design may provide a better result than a harder coating.
Sử dụng các điều kiện ứng dụng để đưa ra danh sách rút gọn hệ thống vật liệu – lớp phủ
The following matrix provides a starting direction, not a final engineering specification.
| Điều kiện ứng dụng | Hướng chất nền để đánh giá | Hướng bề mặt để đánh giá | Xác minh trước |
| Moderate volume, robust geometry, controlled process | D2 / SKD11 hoặc HSS | Polished uncoated surface, TiN, TiCN, or nitriding depending on wear | Grade, Độ dày, Giải phóng mặt bằng, sự bôi trơn |
| Mài mòn khối lượng lớn | HSS, PM steel, hoặc cacbua | Điều trị PVD tập trung vào mài mòn | Căn chỉnh, edge support, regrinding plan |
| Galling với việc thu gom vật liệu có thể nhìn thấy | Thép HSS hoặc PM cứng cáp nếu chất nền vẫn ổn định | Low-friction PVD, DLC-type system, multilayer coating, or nitriding | Kết thúc, chất bôi trơn, Nhiệt, stripper action |
| Cú đấm nhỏ hoặc mảnh có sứt mẻ | Tough HSS, PM steel, or shock-resistant steel | Chỉ phủ sau khi kiểm soát được nguyên nhân gãy | Unsupported length, sự hướng dẫn, các góc, sự căn chỉnh |
| Tấm không gỉ dày hoặc tải trọng cao | HSS or PM steel; carbide only in a rigid, stable setup | Heat- and wear-appropriate coating | Punch load, Giải phóng mặt bằng, hỗ trợ, điều kiện báo chí |
| Môi trường dụng cụ ăn mòn | Thép công cụ không gỉ chống ăn mòn khi tải cho phép | Xử lý tương thích với chất nền không gỉ đã chọn | Khả năng chống ăn mòn hay hiệu suất đục lỗ là ưu tiên hàng đầu |
Do not use this matrix to skip testing or drawing review. Two applications using the same stainless grade may need different punches because the thickness, hole diameter, punch length, sự bôi trơn, tốc độ nhấn, and service expectations are different.
So sánh các tùy chọn công cụ theo khả năng sử dụng và chi phí mỗi lần truy cập
Initial purchase price is a weak basis for comparing punch options.
A more useful evaluation includes:
- hits between sharpening or replacement;
- unplanned downtime;
- tool-change frequency;
- regrinding cost;
- recoating feasibility;
- dimensional loss after sharpening;
- scrap and surface-damage risk;
- inspection time;
- Thời gian giao hàng thay thế;
- probability of sudden fracture.
A PM steel or carbide punch may cost more at the start but reduce cost per hit in a stable application. The same upgrade can become expensive if the punch continues to break because of misalignment or poor guidance.
Regrinding also changes the tool. It can reduce punch length, remove the treated surface near the cutting edge, alter corner geometry, and affect shut height or penetration. Recoating is possible only when enough usable material remains and the surface can be restored to the condition required by the coating supplier.
The service plan should therefore be considered before the original material and coating are selected.
Thông tin cần đưa vào RFQ Punch-Pin tùy chỉnh
A supplier cannot make a defensible recommendation from the phrase “punch for stainless steel” alone.
Include the following information in the request:
- stainless grade and family;
- độ dày tấm;
- temper, độ cứng, or tensile condition;
- part and hole drawing;
- punch diameter, chiều dài, đầu, cán, and corner geometry;
- required dimensional tolerances;
- die clearance where known;
- press type and stroke rate;
- expected production volume;
- target service interval;
- lubricant or dry-running restriction;
- current punch material and hardness;
- current coating or treatment;
- photographs or samples of wear, xe bán tải, mẻ, or breakage;
- regrinding and recoating expectations;
- vật liệu cần thiết, độ cứng, Kích thước, hoặc tài liệu phủ lớp.
SunshinePro states that it supplies standard components and non-standard customized parts processed from customer drawings. Its relevant punch pages list combinations of CNC machining, mài chính xác, EDM, xử lý nhiệt chân không, kích thước tùy chỉnh, HSS, carbide, stainless tool steel, và các lựa chọn phủ được chọn.
These website-confirmed capabilities should still be reviewed against the actual drawing and application. A tolerance or material listed on one product page should not be assumed to apply to every punch geometry.
Nguyên tắc lựa chọn cuối cùng
Use this order when selecting punch pins for stainless steel stamping:
- Identify the stainless grade, điều kiện, Độ dày, and feature geometry.
- Determine whether the current failure is galling, mài mòn, mẻ, Vỡ, hoặc biến dạng.
- Correct alignment, Giải phóng mặt bằng, sự hướng dẫn, Kết thúc, việc lột đồ, and lubrication problems.
- Select the substrate for bulk toughness, độ bền nén, and edge stability.
- Select the coating or treatment for the dominant surface failure.
- Compare serviceability, thời gian ngừng hoạt động, and cost per hit.
- Confirm the final system through drawing review and application-specific validation.
For a custom review, gửi bốc thăm, stainless specification, điều kiện sản xuất, and current failure details through SunshinePro’s Trang liên hệ. That information gives the supplier a practical basis for evaluating the punch material, xử lý nhiệt, Kết thúc, Lớp phủ, và yêu cầu kiểm tra.
Chia sẻ:



Được viết bởi Sunshine
Tại Sunshine, Chúng tôi là nhà sản xuất và cung cấp chuyên nghiệp các linh kiện khuôn chính xác, cung cấp một loạt sản phẩm đa dạng cho ứng dụng dập và khuôn ép. Trọng tâm chính của chúng tôi bao gồm khuôn đục lỗ, ghim và ống lót đẩy, và cọc hướng dẫn cùng các bushing. Với gia công CNC tiên tiến, Kiểm soát chất lượng nghiêm ngặt, và năng lực sản xuất mạnh mẽ, chúng tôi đảm bảo độ tin cậy, các bộ phận chính xác cao, cùng với các linh kiện tiêu chuẩn có sẵn trong kho để cung cấp nhanh chóng và hiệu quả toàn cầu.
TIN TỨC
NHẬN DỊCH VỤ
Với các bộ phận chất lượng đáp ứng mọi ngân sách và đội ngũ nhân viên thân thiện được đào tạo để giúp chuyến thăm của bạn trở nên hữu ích và thuận tiện.
