



Thiết kế đường ngắt máy tính bảng để tách và tuổi thọ dụng cụ đáng tin cậy
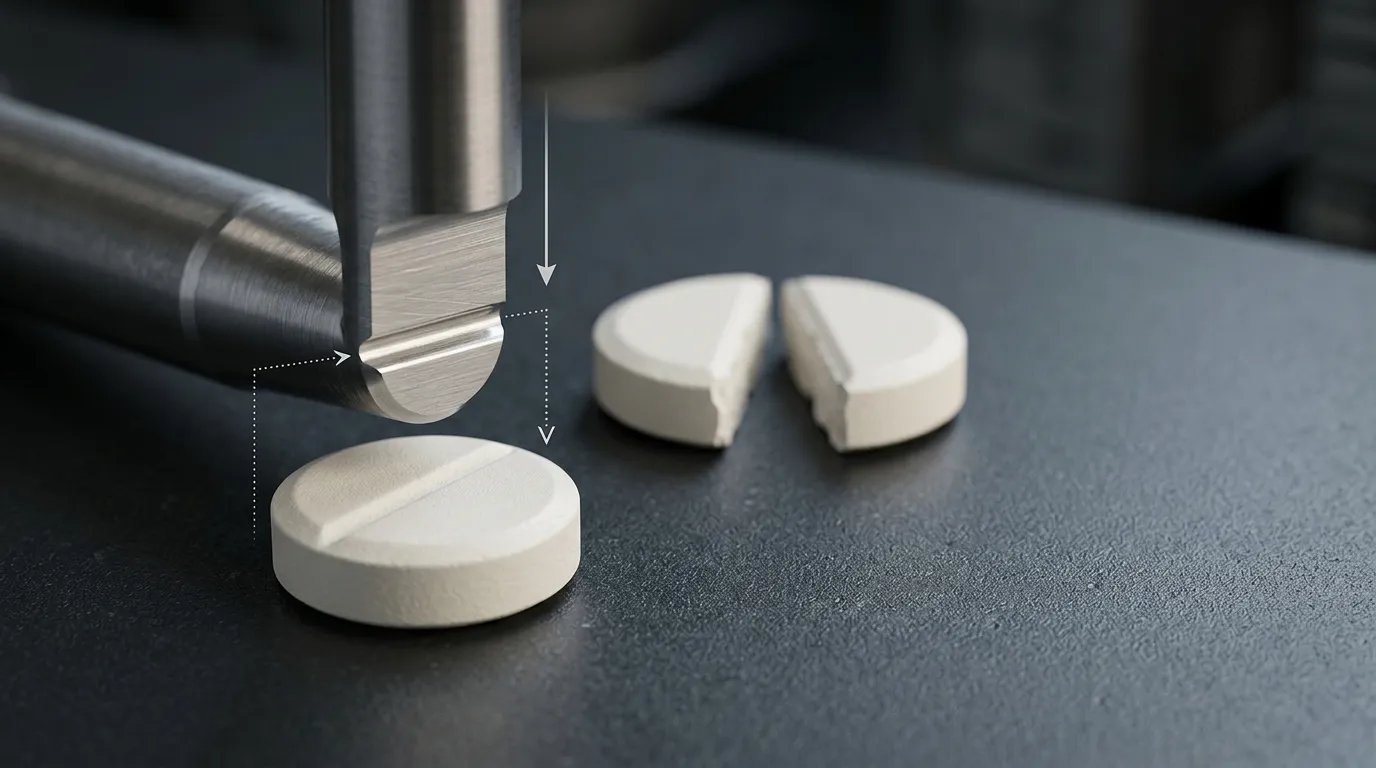
Tablet break line design is not a matter of making the deepest possible groove. A functional break line, also called a tablet score line, must guide the tablet along an intended fracture path while leaving enough strength for compression, sự đẩy ra, Lớp phủ, Bao bì, and handling.
The geometry must also be practical for the punch tip that forms it. A sharper or more protruding feature may help initiate a break, but it can increase local stress, reduce clearance between upper and lower punches, or make the tooling more vulnerable to chipping.
Hình học đường ngắt là một quyết định chuyên biệt trong phạm vi rộng hơn của Các loại dụng cụ ép viên. The final design should be evaluated as a system involving the tablet shape, Độ dày, sự công thức, hardness range, punch configuration, nhấn cài đặt, and product-validation method.
What Makes a Tablet Break Line Functional?
A functional score line is intended to help a tablet divide into defined portions. Its performance cannot be judged only by how visible, straight, or symmetrical the groove appears.
A useful break line should support several outcomes:
- The tablet can be held and divided using the intended method.
- Fracture occurs close to the planned path.
- The resulting portions are reasonably consistent.
- Material loss from crumbs and fragments remains controlled.
- The intact tablet remains strong enough for production and handling.
- Subdivision does not create unacceptable changes in product performance.
Thuộc tính Hướng dẫn của FDA về chấm điểm máy tính bảng treats scoring as a product-performance issue rather than a cosmetic feature. Depending on the product and market, evaluation may include splitting behavior, mass loss, tính dễ vòi, sự tan rã, Sự ổn định, and performance across the proposed tablet-hardness range.
Điểm chức năng so với rãnh trang trí
A tablet may contain a visible groove without being suitable for accurate subdivision. A decorative line may improve appearance or product recognition, but it should not be represented as a functional score unless the finished tablet has been tested for that purpose.
Visual inspection can confirm that the groove exists. It cannot prove that:
- The fragments have consistent mass.
- The active ingredient is evenly distributed.
- The tablet will divide similarly across the production hardness range.
- The split portions retain acceptable release characteristics.
- Patients or operators can reproduce the result using the intended method.
Tooling inspection and tablet-performance validation are therefore separate requirements.
Biến hình học đường ngắt và sự đánh đổi của chúng
A score feature is defined by several connected dimensions. Changing one variable can affect the others, so break-line depth should never be specified in isolation.
| Biến thiết kế | Hiệu quả dự định | Rủi ro nếu đi quá xa | Những gì phải được xác minh |
|---|---|---|---|
| Độ sâu hoặc độ thâm nhập | Giảm phần máy tính bảng phải gãy | Weak intact tablet, fragile center, tall punch feature | Tablet strength, split force, punch clearance |
| Chiều rộng rãnh | Tạo không gian cho điểm số và ảnh hưởng đến hồ sơ của nó | Loại bỏ vật liệu dư thừa hoặc độ nét trực quan kém | Hành vi đứt gãy và khả năng sản xuất |
| Góc bao gồm | Tập trung đường đứt gãy | Hình dạng đục lỗ sắc nét và ứng suất cục bộ cao hơn | Sức mạnh đục lỗ và tính nhất quán của phân chia |
| Bán kính gốc | Kiểm soát độ sắc nét ở cuối điểm số | Too small may weaken the tooling; too large may reduce fracture guidance | Căng thẳng của dụng cụ và khả năng gãy của viên nén |
| Độ dài điểm số | Mở rộng đường đứt gãy có hướng dẫn | Sứt mẻ cạnh hoặc nhiễu các tính năng khác | Đường dẫn vết nứt và bố cục mặt máy tính bảng |
| Vị trí và định hướng | Xác định hình học phân đoạn dự định | Các mặt cắt không bằng nhau hoặc sai lệch | Symmetry, Keying, and drawing orientation |
The correct combination depends on the tablet rather than on a universal score-line standard.
Depth, Width, and Remaining Tablet Section
A deeper groove leaves less tablet material beneath the score. This can reduce the force needed to start a fracture, but it can also weaken the tablet before the user intends to split it.
Depth must be considered relative to:
- Overall tablet thickness.
- Cup depth and face curvature.
- The location of the score across the curved surface.
- Tablet hardness.
- Whether the opposite face also contains a score.
- The height and shape of the punch-tip feature.
Ví dụ, the same nominal score depth may leave a substantial residual section in a thick, shallow-profile tablet but a much thinner section in a smaller tablet with a deep cup.
Groove width also affects the feature profile. It should provide a manufacturable transition without removing more material than necessary or creating a punch feature that is too thin to withstand repeated loading.
Góc và bán kính gốc
The included angle and root radius influence how strongly the score concentrates stress when the tablet is bent.
A sharp groove can encourage fracture to start at the intended line. The corresponding punch-tip feature, tuy nhiên, may contain a thin or sharp transition where mechanical stress becomes concentrated during each compression cycle.
A larger root radius generally creates a smoother tooling transition, but it may provide less concentrated fracture guidance in the tablet. This is why angle and radius should be reviewed together rather than treated as independent cosmetic dimensions.
Các nguồn thiết kế máy tính bảng kỹ thuật như I Giấy thiết kế máy tính bảng Hà Lan discuss score penetration, bán kính, góc, punch stress, and the need to balance tablet breakability with robust tooling. These relationships are useful design principles, but they do not establish a universal dimension for every formulation.
Chiều dài, Chức vụ, and Interaction With Face Features
The score should follow the intended segment boundary and remain compatible with the tablet’s shape and face profile.
Its endpoints require particular attention. A line that extends too close to a tablet edge may create a vulnerable edge condition, while a line that stops too early may not guide the complete fracture path.
Other face features also affect placement:
- Logos and characters can interrupt a symmetrical fracture path.
- Deep embossing can compete with the score for available face area.
- Curved surfaces can change the effective score penetration along its length.
- Off-center placement can create unequal tablet sections.
- Multiple intersecting scores increase both tablet and punch-tip complexity.
The score, identification marks, and overall cup profile should be reviewed as one punch-face layout.
Tại sao thuộc tính máy tính bảng thay đổi kết quả
Identical punch geometry can produce different subdivision behavior in different formulations.
Tablet size and shape influence how the product can be held and where bending forces are applied. A large oblong tablet may provide more leverage than a small round tablet, even when the score geometry appears similar.
Thickness and cup profile determine how much material remains under the groove. Formulation properties then control how that material responds to stress.
Relevant formulation behavior includes:
- Brittleness.
- Phục hồi đàn hồi.
- Biến dạng dẻo.
- Compactability.
- Internal bonding strength.
- Distribution of the active ingredient.
Compression force also changes the result because it influences tablet density and hardness. A score that performs well at one development condition may become difficult to break at a higher hardness or excessively fragile at a lower one.
Đánh giá được bình duyệt Tablet Scoring: Current Practice, Fundamentals, and Knowledge Gaps describes tablet subdivision as a multivariable problem involving patient use, hình học máy tính bảng, sự công thức, manufacturing conditions, and the selected test method.
The design should therefore be evaluated across the intended production range, not only on a single batch produced under ideal development conditions.
Single-Sided or Double-Sided Scoring?
A tablet can be scored on one face or on both opposing faces. Neither configuration is automatically better.
| Yếu tố lựa chọn | Điểm số một chiều | Điểm hai mặt |
| Cấu hình đục lỗ | Tính năng ghi điểm trên một mặt đấm | Các tính năng phối hợp trên cú đấm trên và dưới |
| Căn chỉnh xoay | Thường ít đòi hỏi hơn | Các đối tượng địa lý đối lập phải được căn chỉnh |
| Phần máy tính bảng còn lại | Điều khiển từ một bên | Giảm từ cả hai phía |
| Rủi ro giải phóng mặt bằng | Thấp hơn cho mặt đối phương không ghi điểm | Các phần nhô ra đối diện có thể làm giảm khe hở đầu đục lỗ |
| Độ phức tạp của bố cục khuôn mặt | Để lại mặt đối diện có sẵn | Sử dụng không gian trên cả hai mặt |
| Độ nhạy thiết lập | Nói chung đơn giản hơn | Phụ thuộc nhiều hơn vào khóa và độ dài danh nghĩa |
| Cần xác minh | Sản phẩm cụ thể | Sản phẩm- and setup-specific |
A double-sided score may guide fracture from both surfaces, but it introduces additional mechanical and setup requirements. The two features must be positioned correctly relative to each other, and their combined penetration must not leave an excessively weak central section.
The choice should be based on the tablet geometry, sự công thức, intended segment pattern, available face area, hệ thống dụng cụ, and validation results.
Căn chỉnh và khóa cho điểm số đối lập
Opposed score features must remain rotationally aligned during production. If one punch turns relative to the other, the score lines may no longer meet across the intended fracture plane.
Anti-turn keys and key guides can control punch orientation. Depending on the tooling arrangement, the lower punch may also require a keyed configuration.
The review should confirm:
- Which punch faces contain the score.
- The required angular orientation.
- The location of each key.
- Whether the press supports the intended keyed arrangement.
- How orientation will be checked during setup.
- Whether key or guide wear could allow movement over time.
This discussion is limited to score alignment. General upper- and lower-punch functions belong to the broader tooling system rather than this specific break-line decision.
Bảo vệ đầu đục lỗ khỏi tiếp xúc và hỏng hóc sớm
The score feature machined into a punch face may be narrow, sharp, or raised relative to the surrounding cup. These conditions can increase local mechanical stress.
Repeated compression subjects the punch to cyclic loading. A geometry with a thin section or abrupt transition may become more vulnerable to fatigue, while an overload, contact event, unsuitable material condition, or handling impact can contribute to chipping or brittle fracture.
A Thảo luận về Công nghệ Dược phẩm về lỗi dụng cụ identifies fatigue, brittle fracture, thiết kế đục lỗ, tình trạng vật liệu, and compaction load as relevant contributors to punch-tip damage.
The main tooling risks associated with a break line include:
| Rủi ro | Nguyên nhân có thể | Hậu quả có thể xảy ra | Hành động xem xét |
| Tập trung căng thẳng cục bộ | Sharp angle, small radius, thin feature | Tính năng điểm nứt mỏi hoặc sứt mẻ | Xem lại quá trình chuyển đổi và tải |
| Liên hệ tính năng đối lập | Không đủ khe hở trên / dưới | Sứt mẻ hoặc gãy ngay lập tức | Kiểm tra chiều dài danh nghĩa và khe hở đầu |
| Sai lệch quay | Sự cố khóa hoặc thiết lập | Uneven score, sự can thiệp, poor fracture path | Xác minh điều khiển hướng |
| Phần nhô ra của tính năng dư thừa | Hình học điểm sâu | Nhiễu phóng hoặc giảm khe hở | Xem lại chiều cao tính năng và loại bỏ máy tính bảng |
| Quá tải | Lực nén cao hoặc tình trạng ép bất thường | Biến dạng dẻo hoặc hỏng giòn | Xác nhận phạm vi hoạt động |
| Thiết kế máy tính bảng cận biên | Thâm nhập quá mức hoặc phần trung tâm yếu | Gãy xương viên nén sớm | Thử nghiệm trong các điều kiện sản xuất |
Tool material and heat treatment affect durability, but they cannot compensate for direct punch contact, an unsafe stress concentration, or an incorrect press setup.
SunshinePro của trang dụng cụ báo chí máy tính bảng Danh sách thép tốc độ cao, Gia công CNC, xử lý nhiệt, kiểm tra kích thước, and custom tooling from drawings or samples. These are relevant supplier capabilities, but they should not be interpreted as a guarantee of score performance or tool life for a specific product.
Khoảng trống đục lỗ từ trên xuống dưới
Double-sided or highly protruding score features require careful clearance review.
The available gap depends on more than the visible tablet thickness. It can also be affected by:
- Feature height above each punch face.
- Upper and lower punch nominal lengths.
- Compression position.
- Press adjustment.
- Mài mòn dụng cụ.
- Setup error.
- Deflection under load.
A practical review sequence is:
- Dimension the score features on both punch drawings.
- Confirm the nominal lengths of the upper and lower punches.
- Calculate the minimum expected separation at the operating position.
- Include a suitable safety margin for manufacturing and setup variation.
- Verify the arrangement during installation and trial compression.
- Inspect the punch tips after the trial for evidence of contact.
Press-specific values should come from the press manufacturer, approved tooling drawings, and project calculations rather than from a generic article.
Các vấn đề sản xuất và xử lý liên quan đến điểm số
A scored tablet can survive compression but fail during a later production stage.
Trong quá trình phóng, the lower punch raises the tablet through the die. A weak score area may chip as the tablet moves, while a protruding punch feature may complicate release from the punch face.
Take-off introduces another contact event. If the tablet has already been weakened excessively, lateral movement can cause edge damage or premature fracture.
Coating and packaging can also expose a marginal design:
- Coating may bridge across the groove.
- Coating film may crack when the tablet is divided.
- Tablets may rub against each other during coating and handling.
- Packaging equipment may apply local loads.
- Transport vibration may break tablets that lack sufficient intact strength.
These problems do not prove that the score is always the root cause. The formulation, ejection force, tình trạng dụng cụ, quy trình phủ, packaging design, and handling system may also contribute.
The purpose of the break-line review is to determine whether the score has created an avoidable weak section or tooling feature before wider process changes are made.
Chẩn đoán lỗi trước khi thay đổi đường ngắt
A score redesign should follow evidence, not assumptions.
| Vấn đề quan sát được | Nguyên nhân có thể | Bằng chứng cần thu thập |
| Máy tính bảng khó phân chia | Shallow score, high hardness, unsuitable formulation, poor grip, unsuitable test method | Hardness data, breaking method, segment results |
| Máy tính bảng thoát khỏi điểm số | Misplaced line, formulation fracture pattern, asymmetric geometry | Fracture location, cross-section, tablet dimensions |
| Các mảnh không bằng nhau | Off-center score, rotational misalignment, inconsistent splitting method | Tool orientation, segment mass, user method |
| Chip máy tính bảng trong quá trình đẩy ra | Weak edge, excessive penetration, high ejection force, tình trạng dụng cụ | Ejection data, chip location, punch and die inspection |
| Máy tính bảng tách thành nắp | Mắc kẹt không khí, formulation or compression issue, tooling configuration | Defect plane, press parameters, formulation review |
| Chip tính năng điểm đấm | Direct contact, tập trung ứng suất, quá tải, xử lý hư hại | Tip-gap check, fracture surface, setup records |
Capping should not be treated as another name for a score-related break. A score is intended to guide fracture through a defined plane, while capping usually involves separation of the top or bottom portion of the tablet from the main body.
Where the defect pattern indicates cap separation rather than failure along the intended score, the reader should move to the dedicated Giải pháp dụng cụ đóng nắp máy tính bảng guidance instead of expanding the break-line article into a full capping investigation.
Cách xác nhận thiết kế đường ngắt chức năng
A functional break line requires verification at several levels. Dimensional inspection alone is not enough.
1. Inspect the Tooling
Confirm that the manufactured punches match the approved drawings.
Relevant checks may include:
- Score depth.
- Width.
- Góc bao gồm.
- Bán kính gốc.
- Length and endpoint position.
- Định hướng.
- Vị trí chủ chốt.
- Upper and lower punch nominal lengths.
- Tình trạng bề mặt.
- Opposed-feature clearance.
SunshinePro mô tả báo cáo kiểm tra và kiểm tra kích thước trong Thực hành kiểm soát chất lượng. These checks can verify whether the tool conforms to the specification, but they do not establish how a pharmaceutical formulation will behave.
2. Conduct Representative Press Trials
Trials should use the intended formulation and a relevant operating window.
The trial plan should consider:
- Low and high tablet-hardness conditions.
- Expected compression-force range.
- Production speed where it affects performance.
- Ejection and take-off behavior.
- Tool orientation.
- Evidence of upper/lower punch contact.
- Tablet chipping or premature fracture.
- Repeated-cycle effects on the punch feature.
A single successful compression event does not prove that the design is robust for production.
3. Evaluate the Whole Tablet
Before subdivision, confirm that the scored tablet remains suitable for handling.
Evaluation may include:
- Visual integrity.
- Breaking force or hardness.
- Friability.
- Resistance to coating and packaging damage.
- Stability during normal storage and transport.
- Consistency across batches and operating conditions.
The score should not make the intact tablet so weak that it breaks before the intended use.
4. Evaluate the Split Portions
Subdivision testing should represent the intended method, such as hand splitting or a defined mechanical device.
Depending on the product and regulatory strategy, Đánh giá:
- Ease of splitting.
- Fracture location.
- Segment mass variation.
- Material loss.
- Content uniformity.
- Friability of the resulting portions.
- Dissolution or release behavior.
- Stability of split portions where required.
Equal mass does not automatically prove equal active content. If the formulation contains an uneven distribution of active ingredient, two fragments with similar weight may still differ in drug content.
The FDA guidance is relevant to products intended for the United States. Worldwide projects must confirm requirements in each applicable market, particularly for modified-release products or dosage forms where subdivision may alter release behavior.
Kiểm tra dụng cụ không phải là xác nhận sản phẩm
The responsibility boundary should remain clear:
| Hoạt động | Những gì nó xác nhận | Những gì nó không xác nhận |
| Phê duyệt bản vẽ | Kích thước và cấu hình dự kiến | Hiệu suất máy tính bảng hoàn thiện |
| Kiểm tra dụng cụ | Sự phù hợp với bản vẽ | Phân khu đáng tin cậy |
| Phiên tòa báo chí | Hành vi nén và xử lý trong điều kiện thử nghiệm | Tính nhất quán đầy đủ của lô thương mại |
| Thử nghiệm dược phẩm | Hiệu suất sản phẩm và phân khúc | Tuổi thọ dụng cụ lâu dài trong mọi điều kiện ép |
A tooling supplier can manufacture and inspect a punch feature. The pharmaceutical manufacturer or product owner must validate the final tablet.
Thông tin cần chuẩn bị trước khi đặt hàng dụng cụ máy tính bảng có điểm
A complete enquiry reduces the risk of designing the score without enough product or press information.
Dữ liệu máy tính bảng
Cung cấp:
- Hình dạng viên bảng.
- Diameter or major and minor dimensions.
- Overall thickness.
- Hồ sơ cốc.
- Target number of portions.
- Required segment symmetry.
- Coating status.
- Logos, characters, or other face features.
- Intended hand or mechanical splitting method.
Dữ liệu Break-Line
Define, where already established:
- Single- or double-sided configuration.
- Depth.
- Width.
- Góc bao gồm.
- Bán kính gốc.
- Chiều dài.
- Endpoint position.
- Định hướng.
- Relationship to logos or embossing.
Where the dimensions remain under development, identify them as proposed rather than validated.
Dữ liệu công thức và quy trình
Include relevant information such as:
- Development status of the formulation.
- Intended hardness range.
- Expected compression-force range.
- Known brittleness or elastic-recovery concerns.
- Ejection or take-off issues from prior trials.
- Lớp phủ, Bao bì, and handling requirements.
A tooling supplier does not need the full confidential formulation to understand that the tablet’s fracture behavior and hardness range affect the score design. The level of disclosure can be agreed within the project.
Dữ liệu báo chí và dụng cụ
Xác nhận:
- Press model.
- Tooling standard.
- Punch type.
- Upper and lower punch nominal lengths.
- Keying requirements.
- Key orientation.
- Available lower-punch keying.
- Existing tooling drawings or samples.
- Inspection-document requirements.
SunshinePro tuyên bố rằng họ cung cấp tùy chỉnh dụng cụ ép máy tính bảng from drawings or samples and lists size customization, material-selection support, Gia công CNC, xử lý nhiệt, and dimensional inspection. Final material, hình học, phạm vi kiểm tra, and project suitability should still be confirmed for the specific enquiry.
Nguyên tắc đánh giá thiết kế cuối cùng
Before approving a scored-tablet tooling drawing, confirm five points:
- The score geometry has been reviewed relative to the tablet thickness, hình dáng cốc, sự công thức, and hardness range.
- The selected single- or double-sided configuration matches the intended fracture path.
- Opposed features have adequate alignment and upper/lower punch clearance.
- Nén, sự đẩy ra, take-off, Lớp phủ, Bao bì, and handling risks have been considered.
- The validation plan separates tooling conformance from whole- and split-tablet performance.
There is no universal break-line geometry that guarantees accurate splitting and long tool life. The most reliable approach is to combine a complete tablet specification, a controlled punch-face design, suitable press setup, and product-specific validation.
For a custom tooling enquiry, prepare the tablet drawing, score dimensions, chi tiết báo chí, keying requirements, and requested inspection records before liên hệ với SunshinePro.
Chia sẻ:



Được viết bởi Sunshine
Tại Sunshine, Chúng tôi là nhà sản xuất và cung cấp chuyên nghiệp các linh kiện khuôn chính xác, cung cấp một loạt sản phẩm đa dạng cho ứng dụng dập và khuôn ép. Trọng tâm chính của chúng tôi bao gồm khuôn đục lỗ, ghim và ống lót đẩy, và cọc hướng dẫn cùng các bushing. Với gia công CNC tiên tiến, Kiểm soát chất lượng nghiêm ngặt, và năng lực sản xuất mạnh mẽ, chúng tôi đảm bảo độ tin cậy, các bộ phận chính xác cao, cùng với các linh kiện tiêu chuẩn có sẵn trong kho để cung cấp nhanh chóng và hiệu quả toàn cầu.
TIN TỨC
NHẬN DỊCH VỤ
Với các bộ phận chất lượng đáp ứng mọi ngân sách và đội ngũ nhân viên thân thiện được đào tạo để giúp chuyến thăm của bạn trở nên hữu ích và thuận tiện.
