



Thiết kế chốt đục lỗ đục lỗ cho các mẫu lỗ nhỏ lặp đi lặp lại
Perforation punch pin design is not simply a matter of choosing a small diameter and a hard material. A reliable design must coordinate the hole pattern, sheet material, hình học đục lỗ, support system, combined cutting force, Cuộc Thanh Tra, slug path, and maintenance method.
The challenge becomes greater as hole diameter decreases or more holes are punched during each stroke. A long, unsupported tip may deflect. A dense cluster can exceed press capacity or distort the sheet. Small slugs may clog the die or return to the work surface. The punch therefore has to be designed as part of the complete cutting system.
Để biết thông tin rộng hơn về cú đấm, stripper systems, các phần tử dẫn hướng, and other tooling parts, xem Hướng dẫn thành phần khuôn (được suy luận). This guide focuses specifically on punch pins used for repeated small-hole patterns.
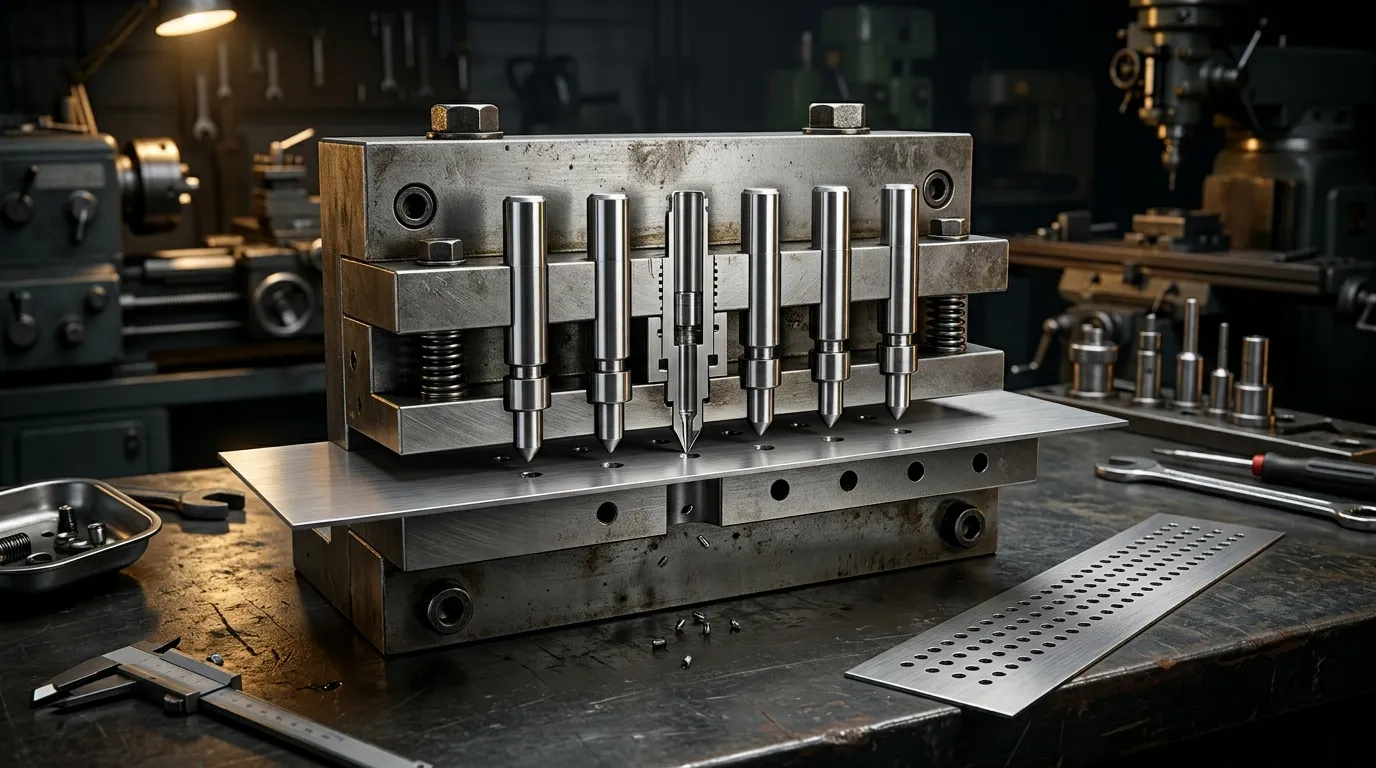
What Must Be Designed Together in a Perforation Punching System?
A perforation punch pin forms one part of a load path that extends through the tool:
- The cutting tip enters the sheet.
- The punch shank transfers the cutting load upward.
- The punch plate locates and retains the pin.
- The backing plate supports the punch against axial reaction.
- The stripper controls the sheet and may guide the punch near its tip.
- The die opening provides the opposing cutting edge.
- The slug passes through the die relief and exits the tool.
A weakness in any one part can affect the entire operation. A strong punch material will not prevent failure if the working tip is too long, the stripper allows lateral movement, or the die opening is misaligned. A correctly sized pin can still produce unstable results if several tips create excessive combined force or if the slug path becomes blocked.
This is why perforation tooling should not be treated as an isolated component-selection exercise. General die construction and die-type decisions are covered more broadly in the Hướng dẫn đục lỗ. Tại đây, the design starts with the repeated hole pattern and works inward toward the punch pin.
Xác định các yêu cầu về mẫu lỗ và tấm trước khi thiết kế chốt
The working diameter is only one input. Before selecting a pin architecture or material, define the conditions that control the cutting operation.
The design package should include:
- Vật liệu và tình trạng tấm
- Độ dày tấm danh nghĩa và dung sai độ dày
- Hole diameter, Hình dạng, and dimensional tolerance
- Bước lỗ theo mỗi hướng
- Vật liệu còn lại giữa các lỗ liền kề
- Pattern arrangement, including aligned or staggered rows
- Khu vực mở bắt buộc
- Hướng gờ và chiều cao gờ cho phép
- Yêu cầu về độ phẳng của tấm
- Khối lượng sản xuất dự kiến
- Công suất báo chí và trạm có sẵn
- Yêu cầu về bôi trơn và độ sạch
- Phương pháp mài và thay thế theo kế hoạch
These inputs are connected. Changing the sheet thickness affects cutting force, slug geometry, practical hole size, and die clearance. Reducing hole pitch leaves less material between adjacent openings and may weaken both the sheet and the die. Increasing the number of tips raises the combined cut perimeter and total force.
Hole Size, Vật chất, and Thickness Set the First Feasibility Check
A small hole is more difficult to punch when its diameter approaches or falls below the sheet thickness. The exact practical limit depends on the work material, punch material, sự hướng dẫn, sự căn chỉnh, tool construction, and required hole quality.
A hard or high-strength sheet generally creates greater cutting load than a softer material of the same thickness. A small punch cross-section must carry that load without bending, mẻ, or breaking. Guided tooling may support a more demanding diameter-to-thickness relationship than a long, non-guided punch, but guidance does not eliminate the need for sufficient punch strength.
Tài liệu tham khảo kỹ thuật như hướng dẫn của MISUMI về đục lỗ đường kính nhỏ emphasize short working sections, stepped support, and controlled slug removal. Supplier ratios can be useful for an early feasibility check, but they should not be treated as universal design limits.
Pitch, Remaining Web, and Flatness Define the Pattern-Level Risk
Hole pitch is the centre-to-centre distance between adjacent perforations. The remaining web, sometimes called the bridge, is the material left between their edges.
A pattern may contain individually feasible holes but still be difficult to manufacture if the web becomes too narrow. Dense perforations can:
- Giảm độ cứng của tấm cục bộ
- Làm yếu vật liệu khuôn giữa các lỗ
- Tăng nguy cơ tương tác lỗ
- Tạo độ căng hoặc độ gợn sóng của tấm
- Tạo hộp dầu trên một bảng điều khiển lớn hơn
- Tập trung tải trọng cắt vào một vùng của dụng cụ
Aligned rows and staggered rows do not distribute load in the same way. A staggered pattern may improve open-area distribution or reduce direct alignment of weak sections, but it does not automatically solve distortion. The finished panel’s flatness requirement must be considered with the complete punching sequence.
Chọn kiến trúc chốt đục lỗ hỗ trợ đầu làm việc nhỏ
A perforation pin normally contains several functional regions:
- Đầu làm việc tạo lỗ
- Chuyển tiếp hoặc vai phía sau đầu
- Một chuôi lớn hơn để truyền và hỗ trợ tải
- Tính năng giữ định vị cú đấm trong tấm đục lỗ
- Phụ cấp điều chỉnh hoặc mài lại khi được yêu cầu
The small working portion should be only as long as the operation needs. Extra unsupported length increases sensitivity to lateral movement and bending. The required length must still allow suitable penetration, stripper guidance, withdrawal, and future sharpening.
Thẳng, Stepped, and Multi-Step Pins Serve Different Section Sizes
| Kiến trúc ghim | Logic thiết kế điển hình | Ưu điểm chính | Hạn chế chính |
|---|---|---|---|
| Ghim thẳng | Tiết diện làm việc và chuôi có tiết diện giống nhau hoặc tương tự nhau | Hình học và sản xuất đơn giản | Một phần có chiều dài đầy đủ rất nhỏ có thể thiếu độ cứng |
| Chốt bước | Đầu làm việc nhỏ được hỗ trợ bởi một chuôi lớn hơn | Hỗ trợ tốt hơn phía sau phần cắt | Vị trí vai và chuyển đổi đòi hỏi thiết kế cẩn thận |
| Ghim nhiều bước | Một số chuyển tiếp kết nối một đầu nhỏ với một cơ thể lớn hơn nhiều | Thay đổi dần dần hơn giữa các phần khác nhau | Hình học và kiểm tra phức tạp hơn |
Thảo luận của MISUMI về Thiết kế đục lỗ distinguishes straight, đã bước, and multi-step punches according to the strength and size of the functional section.
A stepped punch is often considered when the required hole is too small for a long straight pin to remain sufficiently rigid. The larger shank provides support, while the smaller section performs the cut. The transition should transfer load without creating an unnecessarily sharp stress concentration.
Chiều dài làm việc và hình học chuyển tiếp Kiểm soát độ võng và ứng suất
Two punches with the same tip diameter can behave very differently if one has a much longer unsupported working section.
As the slender section becomes longer, the pin becomes more vulnerable to:
- Độ lệch bên
- Sai lệch với lỗ mở khuôn
- Mòn bên không đều
- Sứt mẻ ở lưỡi cắt
- Vỡ mệt mỏi
- Uốn cong trong quá trình tước
The transition behind the working tip also matters. An abrupt reduction in section can create a highly stressed area. A better-supported transition distributes the load into the larger shank while preserving the required access to the sheet and stripper.
There is no single universal working-length ratio for every material and application. The final geometry must account for penetration, độ dày tấm, stripper position, guidance length, regrinding allowance, and the actual load on the tip.
Guide, Giữ lại, and Back the Punch Through the Full Stroke
Small punches require both axial and lateral support.
The punch plate retains and locates the shank. The backing plate supports the punch against cutting reaction. The stripper controls the sheet during withdrawal and may guide the punch close to the cutting region. These elements must remain aligned with the die opening.
Even a correctly dimensioned pin can fail if the support system allows side loading.
Hướng dẫn thoát y hạn chế cú đấm đi lang thang gần đầu cắt
A stripper-guided punch passes through a controlled opening in the stripper plate before entering the sheet. This close support reduces the distance over which the small tip can move laterally.
Lưu ý kỹ thuật của MISUMI về Hướng dẫn thoát y cho các cú đấm lỗ explains that small punches are especially vulnerable to lateral movement. The stripper can reduce that movement, but only when the stripper itself moves accurately.
If the stripper tilts, shifts, or has excessive clearance, it may transfer error to the punch rather than correcting it. The stripper opening, punch shank, and die opening must therefore be treated as one alignment system.
Tấm đục lỗ và tấm lót hoàn thành đường dẫn tải dọc trục
The punch plate positions the pin, but it may not provide sufficient resistance to concentrated axial load by itself. A small punch head or shank can create high local pressure behind the pin.
A backing plate spreads this reaction into a stronger supporting area. Without adequate backing, the punch may indent or sink into the holder, changing its working height and alignment.
Hướng dẫn của MISUMI về Thiết kế tấm lót highlights this issue for punches with small supporting cross-sections.
The load path should remain flat, rigid, and correctly located. A hard punch placed against a weak or poorly supported holder can still lose position under repeated loading.
Khớp số lượng chốt và sắp xếp mẫu với lực đục lỗ có sẵn
A cluster punch produces several holes in one stroke. This can reduce the number of press cycles required, but the press must cut the combined perimeter of all engaged tips.
The total load is not determined by hole count alone. It depends on:
- Tổng chu vi cắt tham gia
- Độ dày tấm
- Khả năng chống cắt vật liệu gia công
- Số đầu cắt đồng thời
- Độ sắc nét của cú đấm
- Giải phóng mặt bằng
- Điều kiện tước
- Hiệu quả của dụng cụ và máy ép
Adding more tips may increase output per stroke, but it also raises cutting load, slug volume, maintenance exposure, and the possibility of sheet distortion.
Estimate Force from Total Cut Perimeter, Not Hole Count Alone
A conceptual punching-force relationship is:
Lực đục lỗ ≈ tổng chu vi cắt × độ dày tấm × khả năng chống cắt vật liệu
For a cluster, the total cut perimeter is the sum of the perimeters of all tips engaged during the same part of the stroke.
This means ten small round holes do not create the same load as ten slots with a much greater combined perimeter. Two patterns with similar open area may also require different force because their edge lengths differ.
Của Mate Precision Hướng dẫn đục lỗ cụm uses total cutting perimeter as a central force-planning factor and recommends checking cluster load against the machine and station limits.
The calculation should be treated as an engineering estimate. The actual tool must also account for stripping force, load balance, điều kiện báo chí, and the manufacturer’s tooling limits.
Xếp xen kẽ và phân phối tải có thể làm giảm các vấn đề ở cấp độ mẫu
If every adjacent tip enters the material at the same time, cutting load may be concentrated within a small area. This can increase peak force and stretch the sheet around the pattern.
Possible design responses include:
- Chia mẫu trên nhiều trạm
- Sử dụng ít mẹo hoạt động hơn
- Sắp xếp các hàng để phân phối mức độ tương tác
- Chiều dài đầu so le khi hệ thống dụng cụ cho phép
- Cân bằng mẫu xung quanh tâm công cụ
- Thay đổi trình tự đục lỗ
These methods can reduce local concentration, but they may also add tool complexity or change the loading sequence. They must preserve the finished hole locations and part geometry.
Thông tin của Wilson Tool về Đục lỗ bằng các công cụ cụm also identifies sheet stretch and oil-canning as practical concerns in dense perforation work.
Phối hợp giải phóng mặt bằng với sơ tán sên
The punch and die opening form one cutting pair. Clearance between them influences cutting load, fracture behaviour, sự hình thành răng cưa, mòn dụng cụ, and slug release.
Repeated small-hole patterns make waste handling especially important. A cluster with 20 tips creates 20 slugs during each complete punching cycle. Even when each slug is small, the cumulative waste flow can become substantial.
The die must provide:
- Giải phóng mặt bằng cắt phù hợp
- Đầy đủ đất nước
- Cứu trợ bên dưới lưỡi cắt
- Một lối thoát liên tục
- Truy cập để kiểm tra và làm sạch
- Bảo vệ chống lại sự tuần hoàn của sên
Clearance Must Be Verified for the Material, Độ dày, and Required Edge
Clearance is normally considered per side between the punch and die cutting edges. The appropriate value depends on the sheet material, Độ dày, required edge condition, punch condition, and tooling method.
Clearance that is too small may increase force and wear. Clearance that is too large may increase burrs, edge rollover, hoặc biến đổi kích thước. As the punch and die wear, effective clearance changes even if the original dimensions remain correct.
For this article, the important point is that the pin diameter cannot be finalized independently from the die opening. Exact clearance values require material- and application-specific calculation and validation.
Mỗi lỗ bổ sung sẽ thêm một con sên khác phải thoát ra một cách đáng tin cậy
Small slugs can:
- Tích lũy trong các đoạn chết bị hạn chế
- Cầu qua các đoạn phù điêu hẹp
- Nén chặt vào tắc nghẽn
- Dính vào mặt đục lỗ
- Quay trở lại bề mặt làm việc
- Làm hỏng tấm trong lần đột quỵ sau đó
The die relief should allow slugs to move away without trapping one another. Tool access should permit cleaning before debris raises the cutting load or damages the punch.
Slug pulling requires particular attention. A slug that follows the punch upward may be pressed back into the sheet or trapped between the tool and workpiece. Hình học, Giải phóng mặt bằng, sự bôi trơn, điều kiện bề mặt, and waste-path design can all influence this behaviour.
Chọn vật liệu chốt và xử lý bề mặt theo chế độ lỗi dự kiến
The hardest available punch material is not automatically the best choice. Material selection should respond to the dominant failure risk.
Common risks include:
- Abrasive wear
- Mòn hoặc mài mòn chất kết dính
- Sứt mẻ cạnh
- Vỡ mệt mỏi
- Biến dạng dẻo
- Tác động từ sai lệch
- Ăn mòn hoặc hư hỏng bề mặt
A material that resists wear well may be less tolerant of shock or side loading. A tougher material may survive misalignment better but require more frequent sharpening.
thép dụng cụ, HSS, and Carbide Balance Wear and Toughness Differently
| Gia đình vật liệu | Đặc điểm hữu ích | Mối quan tâm thiết kế chính |
| Thép công cụ | Broad balance of toughness, khả năng chống mài mòn, xử lý nhiệt, and regrindability | Hiệu suất phụ thuộc nhiều vào cấp độ và xử lý nhiệt |
| Thép tốc độ cao hoặc luyện kim bột | Có thể cung cấp khả năng chống mài mòn cao hơn trong khi vẫn giữ được độ dẻo dai hữu ích | Chi phí và độ khó gia công có thể tăng lên |
| Cacbua | Khả năng chống mài mòn và cường độ nén cao | Nhạy cảm hơn với tác động, mẻ, and alignment errors |
Carbide may be suitable for stable, chất mài mòn, high-volume applications, but it is not a universal solution for every small hole. A slender carbide tip exposed to side load or impact may chip where a tougher steel punch would survive.
The selection should consider the sheet material, working-tip diameter, chiều dài không được hỗ trợ, sự hướng dẫn, sự bôi trơn, điều kiện báo chí, and previous failure history.
SunshinePro của chốt đục lỗ tùy chỉnh danh sách trang SKH51, SKH9, DC53, ASP-grade materials, and carbide among its stated material options. Final suitability still has to be confirmed against the actual drawing and application.
Bề mặt hoàn thiện, Lớp phủ, and Lubrication Address Surface Interaction
Surface finish influences friction, thu gom vật liệu, Phát hành, and the condition of the substrate beneath a coating. A smoother working surface may help reduce adhesion in suitable applications, but finish alone cannot correct an unsupported tip or misaligned die.
Coatings such as TiN, TiCN, and DLC may be considered for selected wear or friction conditions. Their value depends on:
- Đục lỗ nền
- Vật liệu phôi
- Chuẩn bị bề mặt
- Hình học cạnh
- Bôi trơn
- Nhiệt độ
- Tác động và tải bên
- Độ bám dính của lớp phủ
A coating should not be used as a structural repair. It cannot compensate for excessive working length, poor stripper guidance, weak backing, or incorrect clearance.
Lubrication is also part of the system. It can reduce friction, mài mòn do keo dán, and stripping resistance, but the lubricant must be compatible with the work material, downstream process, and cleanliness requirements.
Design the Tool for Replacement, Mài sắc, and Inspection
Perforation tooling should be serviceable before the first production run begins. A design that performs well initially but cannot be repaired economically may create unnecessary downtime later.
The maintenance plan should address:
- Thay thế chốt riêng lẻ
- Tính khả dụng của đầu tip dự phòng
- Trợ cấp mài sắc
- Điều chỉnh độ dài sau khi mài lại
- Truy cập vào các chân được giữ lại
- Nhận dạng tiền boa
- Điểm kiểm tra
- Giới hạn thay thế
Các công cụ nhiều đầu cố định và các đầu có thể thay thế tạo ra các mô hình bảo trì khác nhau
A fixed multi-tip punch may be compact and mechanically simple. If one tip is damaged, tuy nhiên, the repair may affect the complete tool.
Replaceable-tip systems allow individual punches to be changed without discarding the whole cluster body. Wilson Tool describes replaceable configurations among its perforation-tool options.
Replaceable tips are not suitable for every pattern. Very close spacing may leave insufficient room for individual retention features. The design must also provide access for removal, accurate location after replacement, and a practical spare-parts system.
The best configuration depends on pattern density, Tần suất bảo trì, tool size, and the cost of replacing one damaged position compared with servicing the complete assembly.
Mài lại thay đổi nhiều hơn lưỡi cắt
Sharpening removes material from the cutting face. This changes the punch length and may alter penetration, sự điều chỉnh, stripper relationship, or the available guided length.
Sau khi nghiền lại, Kiểm tra:
- Đường kính hoặc cấu hình đầu
- Tình trạng tiên tiến
- Chiều dài làm việc còn lại
- Độ thẳng
- Độ đồng tâm giữa đầu và chuôi
- Điều kiện chuyển tiếp
- Hư hỏng bề mặt
- Tính năng lưu giữ
- Chiều dài tổng thể hoặc vị trí điều chỉnh
A pin should not remain in service merely because its edge can still be sharpened. If the remaining geometry no longer provides sufficient support or alignment, replacement may be safer than another regrind.
Chẩn đoán các vấn đề về mẫu bằng cách xem xét biến thiết kế đằng sau chúng
Production symptoms rarely identify one guaranteed root cause. They do indicate which design relationships should be checked first.
| Triệu chứng sản xuất | Nguyên nhân thiết kế có thể xảy ra | Các mục cần xem xét |
| Đấm lang thang hoặc thay đổi vị trí lỗ | Long unsupported tip, weak stripper guidance, sai lệch | Chiều dài làm việc, stripper clearance, căn chỉnh tấm biển, tính đồng tâm |
| Đứt gãy nhiều lần | Excessive force, tải bên, tập trung ứng suất, độ dai không đủ | Tip length, sự chuyển tiếp, Vật chất, Giải phóng mặt bằng, press alignment |
| Sứt mẻ cạnh | Brittle material, tác động, poor edge condition, tiếp xúc không đều | Lớp vật liệu, xử lý nhiệt, punch face, sự căn chỉnh |
| Gờ phát triển nhanh chóng | Punch or die wear, changing effective clearance | Cutting edges, Khai trương, sharpening interval |
| Galling hoặc nhặt vật liệu | Vật liệu dán làm việc, poor finish, unsuitable lubrication | Bề mặt hoàn thiện, Lớp phủ, chất bôi trơn, Giải phóng mặt bằng |
| Kéo sên | Độ bám dính, khoảng cách không phù hợp, poor release conditions | Mặt đục lỗ, Khai trương, chất bôi trơn, slug path |
| Sự tắc nghẽn | Hạn chế giải thoát hoặc tích tụ sên quá mức | Quốc gia, sự giải thoát, exit path, cleaning access |
| Các lỗ không đồng đều trên một cụm | Unbalanced load, different tip lengths, độ lệch mảng | Tip projection, backing support, tool rigidity |
| Độ gợn sóng của tấm hoặc đóng hộp dầu | Dense pattern, concentrated engagement, insufficient web | Pitch, pattern sequence, active tip count |
| Tải trọng báo chí quá mức | Too much simultaneous cut perimeter, dull edges, dọn dẹp kém | Pin count, cutting perimeter, Vật chất, điều kiện cạnh |
For a broader review of fractured or chipped punches, Xem đục lỗ đứt gãy trong khuôn dập. The focus here should remain on the design variables created by small diameters and repeated patterns.
Chuẩn bị gói RFQ và bản vẽ sẵn sàng cho nhà cung cấp
A supplier cannot evaluate a perforation application from the punch diameter alone. The same nominal pin may behave very differently in thin aluminium, high-strength steel, tấm phủ, or a dense multi-tip cluster.
Một gói RFQ hữu ích nên bao gồm:
- Vật liệu và tình trạng phôi
- Độ dày danh nghĩa và dung sai
- Hole shape, Kích thước, và dung sai
- Bản vẽ mẫu đầy đủ
- Quảng cáo chiêu hàng và web còn lại
- Hướng gờ yêu cầu
- Yêu cầu về độ phẳng hoặc biến dạng
- Ý định một đầu hoặc công cụ cụm
- Đường kính và chiều dài đầu làm việc
- Kích thước chuôi
- Hình học bước và chuyển tiếp
- Phương pháp lưu giữ
- Die-opening and clearance information, if already defined
- Loại báo chí và công suất liên quan
- Khối lượng sản xuất
- Điều kiện bôi trơn
- Lịch sử lỗi hiện tại cho các dự án thay thế
- Vật liệu yêu cầu và xử lý nhiệt
- Yêu cầu hoàn thiện bề mặt hoặc lớp phủ
- Đặc điểm kiểm tra bắt buộc
- Chiến lược mài lại và pin dự phòng
- Tiêu chí chỉnh sửa và nghiệm thu bản vẽ
Include the Pattern, Báo chí, and Failure History—not Only the Pin Diameter
For a replacement project, provide the complete pattern and production context wherever possible. Useful supporting information may include:
- Hình ảnh cú đấm bị mòn hoặc gãy
- Hình ảnh của tấm bị hư hỏng
- Vị trí của các lỗi trong mẫu
- Lịch sử mài sắc hiện tại
- Tiến triển gờ
- Bằng chứng tắc nghẽn sên
- Thay đổi tải báo chí
- Kích thước đục lỗ và khuôn hiện có
This information helps distinguish a material problem from a geometry, sự căn chỉnh, Giải phóng mặt bằng, or waste-flow problem.
Xác nhận phạm vi sản xuất và tiêu chí chấp nhận trước khi sản xuất
The RFQ should state whether the supplier is being asked to:
- Sản xuất ghim theo bản vẽ đã được phê duyệt
- Đánh giá khả năng sản xuất của hình học chốt
- Đề xuất vật liệu hoặc lớp phủ
- Sản xuất chân thay thế từ mẫu
- Cung cấp tài liệu kiểm tra
- Tham gia vào thiết kế khuôn hoặc ứng dụng rộng hơn
These are different scopes of responsibility.
SunshinePro tuyên bố rằng họ sản xuất chốt đục lỗ tùy chỉnh from customer drawings and lists CNC machining, EDM, mài chính xác, xử lý nhiệt, and optional coatings on the product page. Project-specific material, sự khoan dung, Kết thúc, coating suitability, and inspection requirements should still be confirmed against the drawing.
For a technical review or quotation, provide the pattern drawing, sheet material and thickness, hình học đục lỗ, press information, and any current failure details through the Trang liên hệ SunshinePro.
Chia sẻ:



Được viết bởi Sunshine
Tại Sunshine, Chúng tôi là nhà sản xuất và cung cấp chuyên nghiệp các linh kiện khuôn chính xác, cung cấp một loạt sản phẩm đa dạng cho ứng dụng dập và khuôn ép. Trọng tâm chính của chúng tôi bao gồm khuôn đục lỗ, ghim và ống lót đẩy, và cọc hướng dẫn cùng các bushing. Với gia công CNC tiên tiến, Kiểm soát chất lượng nghiêm ngặt, và năng lực sản xuất mạnh mẽ, chúng tôi đảm bảo độ tin cậy, các bộ phận chính xác cao, cùng với các linh kiện tiêu chuẩn có sẵn trong kho để cung cấp nhanh chóng và hiệu quả toàn cầu.
TIN TỨC
NHẬN DỊCH VỤ
Với các bộ phận chất lượng đáp ứng mọi ngân sách và đội ngũ nhân viên thân thiện được đào tạo để giúp chuyến thăm của bạn trở nên hữu ích và thuận tiện.
