



Dung sai pin định vị khuôn để căn chỉnh lặp lại
There is no single mold positioning pin tolerance that works for every mold. Repeatable alignment depends on a complete tolerance chain: the pin diameter, the mating hole or bushing diameter, the fit between them, the position and orientation of both features, and the dimensional changes that occur during operation.
A pin can be ground to a very tight diameter tolerance and still fail to locate the mold correctly if its hole is misplaced, its axis is tilted, or two locating pins create an overconstrained pattern. For broader guidance on guide systems, mặc, and fit selection, Xem chốt khuôn và ống lót (được suy luận). This guide focuses specifically on defining, calculating, documenting, and inspecting positioning-pin tolerances.
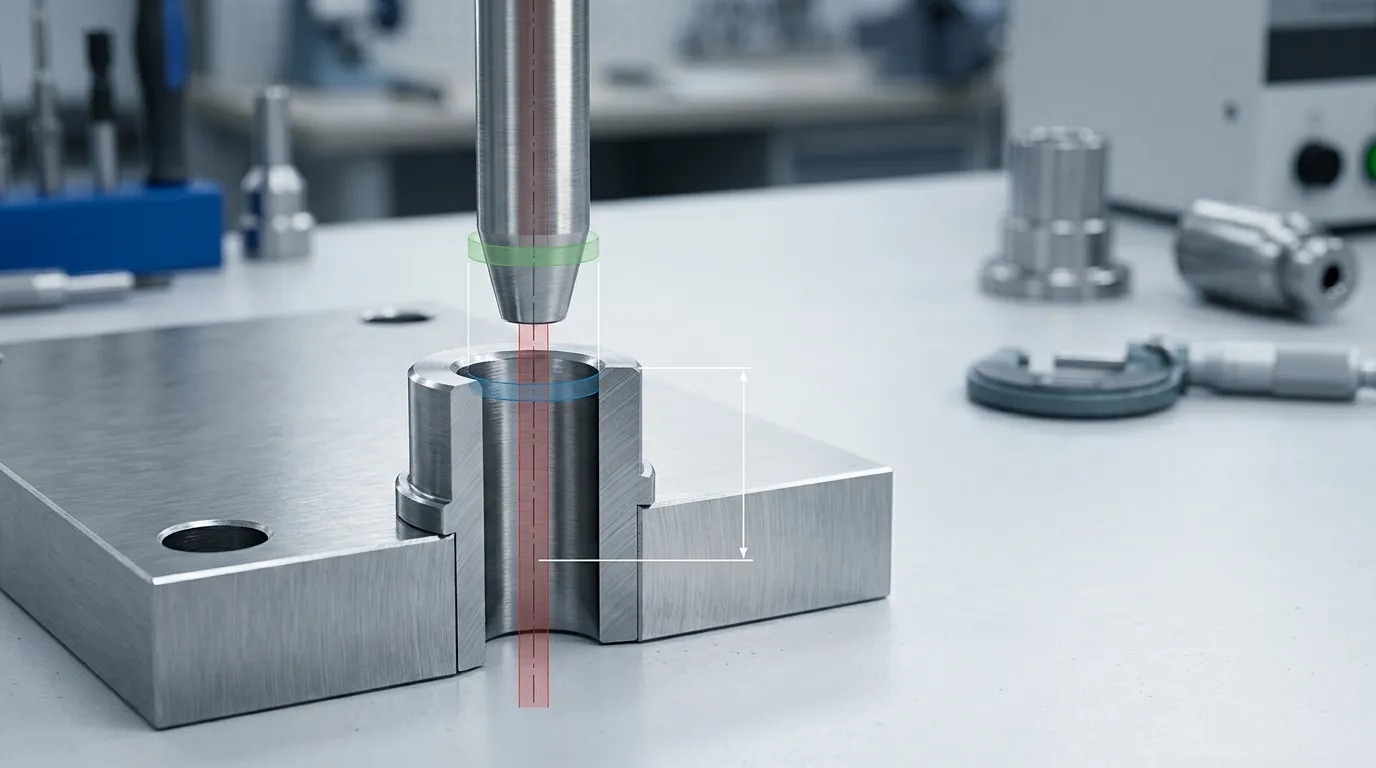
What Does a Mold Positioning Pin Tolerance Actually Control?
The word “tolerance” may refer to several different requirements. These controls are related, but they are not interchangeable.
| Điều khiển | Nó định nghĩa gì | Những gì nó không định nghĩa |
|---|---|---|
| Dung sai kích thước pin | Đường kính chốt lớn nhất và nhỏ nhất có thể chấp nhận được | Vị trí của trục chốt |
| Dung sai lỗ hoặc ống lót | Lỗ giao phối lớn nhất và nhỏ nhất có thể chấp nhận được | Lỗ khoan có được định vị chính xác hay không |
| Phù hợp với lỗ | Khoảng trống hoặc nhiễu có thể xảy ra giữa hai tính năng | Tổng lỗi căn chỉnh khuôn |
| Dung sai hình học | Vị trí và hướng cho phép của trục chốt hoặc lỗ | Khe hở thực tế giữa các bộ phận |
| Độ lặp lại của hệ thống | Khuôn trở lại vị trí cũ một cách nhất quán như thế nào | Liệu vị trí lặp lại đó có phải là vị trí danh nghĩa chính xác hay không |
Thuộc tính Hệ thống giới hạn và phù hợp ISO 286-1 defines size tolerances and fit relationships for holes and shafts. It does not control where a hole is located or whether its axis is perpendicular to the mold plate. Those requirements need geometric controls, such as those defined by Tiêu chuẩn ISO 1101.
Size Tolerance, Vừa vặn, and Alignment Are Different Requirements
Suppose a positioning pin and its mating hole are both within their specified diameter limits. That confirms only that their sizes are acceptable.
It does not confirm that:
- the pin and hole centers coincide;
- their axes are parallel;
- two locating holes have the correct spacing;
- the mold returns to its intended position;
- the assembly will still engage after heating or wear.
The actual fit comes from the combination of both size ranges. The smallest permitted hole paired with the largest permitted pin creates the tightest possible assembly. The largest hole paired with the smallest pin creates the loosest possible assembly.
Both extremes must be checked.
Chức vụ, Định hướng, and Repeatability Complete the Specification
A bore may have the correct diameter but still be offset from its basic location. A pin may be positioned correctly at the plate surface but tilted enough to bind over a long engagement length.
A complete positioning specification may therefore need:
- a functional datum reference frame;
- basic dimensions locating the pin or hole;
- positional tolerance;
- perpendicularity or another orientation control;
- pattern control for multiple locating features.
Repeatability and accuracy should also be distinguished. Repeatability describes how consistently the mold returns to the same position. Accuracy describes how close that position is to the intended nominal location.
A locating system can be repeatable but consistently offset if the feature pattern was manufactured in the wrong position.
Các chân định vị không được tự động coi là tương đương với chốt hướng dẫn khuôn. Guide pins primarily control movement as mold halves open and close. A dedicated positioning pin may establish a more precise final location after the mold halves approach engagement.
Xác định yêu cầu chức năng trước khi chọn phù hợp
A tolerance should start with the required function, not with a familiar fit designation.
Before assigning limits, định nghĩa:
- The maximum permitted translational alignment error.
- The maximum permitted angular error.
- The nominal pin diameter and engagement length.
- Whether the pin is permanent, removable, or replaceable.
- How often the mold will be assembled or disassembled.
- Which side retains the pin.
- Which side provides the locating engagement.
- The operating temperature range.
- The expected wear, sự bôi trơn, and contamination conditions.
- The manufacturing and inspection methods available.
- Whether binding or excess clearance creates the greater functional risk.
A positioning system used for a removable insert may prioritize easy engagement and interchangeability. A permanently installed locator may require stronger retention on its mounting side. A heated mold may need enough room for differential thermal expansion between the pin, bushing, and mold plate.
Application labels alone do not determine the correct fit. An “automotive mold” or “medical mold” still needs a defined alignment requirement, material combination, temperature range, và kế hoạch kiểm tra.
Tách giao diện cố định khỏi giao diện định vị
The two ends of a positioning pin usually perform different jobs.
| Giao diện | Chức năng chính | Hướng phù hợp có thể |
| Mặt gắn | Giữ chốt trong tấm đỡ và bảo toàn trục của nó | Controlled transition or interference, depending on design |
| Định vị bên | Đi vào lỗ giao phối hoặc ống lót và hạn chế chuyển động tương đối | Controlled clearance or transition, depending on function |
Using the same fit on both sides can create avoidable problems. A locating-side interference fit may prevent normal assembly. Excessive mounting-side clearance may allow the pin to shift or loosen.
The final selection must also consider plate thickness, surrounding material, phương pháp loại bỏ, replacement needs, and the risk of distortion during installation.
Chọn phù hợp và tính toán khoảng trống thực tế
Giải phóng mặt bằng, sự chuyển tiếp, and interference fits describe the relationship between the complete pin and hole tolerance zones.
Giải phóng mặt bằng, Chuyển tiếp, and Interference Serve Different Functions
| Loại phù hợp | Kết quả kích thước | Sử dụng chức năng điển hình | Rủi ro chính |
| Phù hợp giải phóng mặt bằng | Lỗ nhỏ nhất vẫn lớn hơn chốt lớn nhất | Tham gia định vị trượt hoặc có thể tháo rời | Chuyển động quá mức nếu khe hở quá lớn |
| Phù hợp với chuyển tiếp | Some valid combinations have clearance; others have interference | Đóng vị trí hoặc giữ chân vừa phải | Lực lắp ráp thay đổi |
| Phù hợp với nhiễu | Chốt nhỏ nhất vẫn lớn hơn lỗ lớn nhất | Lưu giữ vĩnh viễn hoặc bán vĩnh viễn | Biến dạng, loại bỏ khó khăn, hoặc hư hỏng lắp đặt |
These categories describe outcomes, not universal recommendations. A clearance fit may be suitable on the locating side while an interference or transition fit is used on the mounting side.
The hole-basis system is common because standard hole-making tools can establish a defined hole tolerance while the shaft or pin tolerance is selected to create the required fit. Vẫn vậy, a designation such as H7/g6 or H7/m6 is incomplete without the nominal diameter and governing standard. The numerical deviations change across diameter ranges.
Sử dụng kích thước giới hạn để kiểm tra cả hai cực đoan lắp ráp
Calculate the limits before approving the fit.
Giải phóng mặt bằng tối thiểu
Minimum clearance = Smallest permitted hole − Largest permitted pinGiải phóng mặt bằng tối đa
Maximum clearance = Largest permitted hole − Smallest permitted pinA negative result represents interference.
Consider a hypothetical example:
| Đặc tính | Đường kính tối thiểu | Đường kính tối đa |
| Định vị lỗ | 10.010 mm | 10.018 mm |
| Pin định vị | 9,998 mm | 10.004 mm |
The tightest possible assembly is:
10.010 − 10.004 = 0.006 mm minimum diametral clearanceThe loosest possible assembly is:
10.018 − 9.998 = 0.020 mm maximum diametral clearanceThese values are examples only. They are not recommended SunshinePro specifications or universal mold tolerances.
Diametral clearance also should not be treated as the complete alignment error. In an ideal single-pin interface, the pin center may move radially by up to approximately half the diametral clearance before contact. The actual mold position also depends on the second locator, feature positions, axis angles, engagement lengths, biến dạng, và điều kiện vận hành.
Control the Locating Pattern, Not Only the Pin Diameter
A precision fit cannot compensate for an incorrectly located pattern.
The pin and mating feature must be controlled from datums that represent how the mold is assembled and functions. These may include a seating face, a side reference, or another stable mold-base feature.
Use Functional Datums, Chức vụ, and Axis Control
A practical drawing should identify:
- the surfaces establishing the functional datum reference frame;
- the basic locations of the pin and mating hole;
- the permitted positional variation;
- any required perpendicularity or axis-orientation control;
- the relationship between multiple locating features.
Tiêu chuẩn ISO 5458 provides complementary rules for pattern specifications under the ISO GPS system. Drawings using ASME conventions should follow ASME Y14.5.
The drawing should clearly use one governing convention. Mixing ISO and ASME symbols or assumptions without clarification can create conflicting interpretations between the designer, manufacturer, and inspector.
Tránh bị ràng buộc quá mức với một cặp pin tròn và nhẹ nhõm
Two fully round pins entering two close-fitting round holes can overconstrain the assembly.
For both pins to engage, the distance between the pins must agree closely with the distance between the mating holes. Even when every individual diameter is acceptable, accumulated spacing and position variation can cause binding.
A common locating arrangement uses:
- one round pin as the primary locator;
- one diamond, được nhẹ nhõm, or flattened pin as the secondary locator.
The round pin controls movement in two planar directions. The relieved pin controls the required secondary direction while allowing some variation along the relieved axis.
The secondary pin must be oriented correctly. Rotating its relieved direction by 90 degrees changes which movement it permits and which movement it controls.
Locator spacing also affects angular definition. Greater spacing can reduce angular movement for a given amount of linear clearance, but no universal spacing rule applies. Kích thước đĩa, tải trọng, available space, hole-position capability, and engagement geometry still need evaluation.
Xây dựng ngăn xếp dung sai trong trường hợp xấu nhất để căn chỉnh lặp lại
The fit calculation covers only one part of the positioning system. A complete tolerance budget should include every variation capable of moving, tilting, or preventing engagement between the mold halves.
Typical contributors include:
| Người đóng góp | Hiệu quả có thể xảy ra |
| Đường kính pin | Thay đổi giải phóng mặt bằng hoặc nhiễu |
| Lỗ hoặc lỗ lót | Thay đổi giải phóng mặt bằng hoặc nhiễu |
| Vị trí lắp chốt | Di chuyển trục định vị |
| Vị trí lỗ giao phối | Di chuyển trục nhận |
| Hướng trục | Tạo ra sự không khớp góc hoặc tiếp xúc cạnh |
| Ống lót phù hợp với đường kính ngoài | Cho phép hoặc hạn chế chuyển động của ống lót |
| Mối quan hệ nhàm chán với bên ngoài | Bù đắp lỗ ống lót chức năng |
| Khoảng cách mẫu ghim | Ảnh hưởng đến tương tác đồng thời |
| Nhiệt độ tấm khuôn | Thay đổi kích thước thành phần |
| Mặc | Tăng khả năng giải phóng mặt bằng hiệu quả |
| Mảnh vỡ | Giảm khoảng trống có thể sử dụng hoặc ngăn chặn chỗ ngồi đầy đủ |
| Độ không đảm bảo đo lường | Giảm niềm tin vào quyết định chấp nhận |
A practical worst-case process is:
- Define the maximum permitted alignment variation.
- Identify each dimensional and geometric contributor.
- Calculate the tightest and loosest component fits.
- Add the possible positional and orientation effects.
- Check whether every permissible combination can assemble.
- Reserve allowance for operating temperature, mặc, and contamination.
- Confirm that the inspection system can verify the specified limits.
Worst-case analysis is appropriate when assembly must be guaranteed at every permitted limit. Statistical tolerance analysis may be useful in established, capable production processes, but it should not replace functional verification without a justified process model.
Biến thể sản xuất tách biệt với biến thể hoạt động
Manufacturing variation includes:
- component diameter;
- hole diameter;
- vị trí đặc trưng;
- tính vuông góc;
- pattern spacing;
- bushing installation position.
Operating variation includes:
- giãn nở nhiệt;
- mặc;
- mảnh vụn;
- điều kiện bôi trơn;
- plate movement or deformation.
A fit that works during inspection at room temperature may become too tight after heating. A fit that begins with acceptable clearance may lose repeatability as the pin or bushing wears.
Lubrication can reduce friction and seizure risk, but it cannot correct an invalid tolerance stack. Material and hardness affect how well the components retain their dimensions over time, but those decisions should remain separate from the basic fit calculation.
Sử dụng ngăn xếp giả định để kiểm tra thiết kế
Assume a design permits 0.030 mm of total lateral variation at a functional location.
A simplified hypothetical budget might allocate:
| Người đóng góp | Hiệu lực được phép |
| Chuyển động xuyên tâm pin-to-bushing | 0.008 mm |
| Biến thể vị trí ghim | 0.006 mm |
| Biến thể vị trí ống lót | 0.006 mm |
| Định hướng và hiệu quả tương tác | 0.004 mm |
| Nhiệt độ và phụ cấp hao mòn | 0.004 mm |
| Biên độ thiết kế còn lại | 0.002 mm |
If the calculated worst-case total exceeds 0.030 mm, the design must change. Possible actions include:
- reducing maximum clearance;
- improving positional control;
- increasing locator spacing;
- using a replaceable bushing;
- revising the relieved-pin geometry;
- reducing operating variation;
- redefining the functional requirement.
The example demonstrates the budgeting method only. Real values must come from the mold’s geometry, điều kiện vận hành, and manufacturing capability.
Ghi rõ yêu cầu trên bản vẽ hoặc RFQ
A supplier cannot reliably manufacture or inspect an ambiguous precision requirement.
The drawing or request for quotation should identify:
- nominal pin, hole, and bushing dimensions;
- limit dimensions or an unambiguous fit designation;
- the governing tolerance standard;
- separate mounting-side and locating-side requirements;
- dữ liệu chức năng;
- basic feature locations;
- position and orientation tolerances;
- primary and secondary locator roles;
- the orientation of any relieved or flattened pin;
- material and hardness where functionally necessary;
- điều kiện xử lý nhiệt;
- surface finish on locating diameters;
- operating temperature assumptions;
- whether components must be interchangeable;
- whether selective assembly is permitted;
- required inspection characteristics;
- required inspection records;
- whether pins and bushings are supplied as matched components.
The supplier should also know which characteristics are function-critical. A tight pin diameter may be less valuable than a slightly wider size tolerance combined with better positional control.
Tránh các ghi chú chính xác mơ hồ
Specifications that need clarification include:
- “high-precision pin” without dimensional limits;
- “±0.005 mm” without naming the controlled feature;
- an ISO fit class without a nominal diameter;
- pin diameter tolerance without a mating-hole tolerance;
- diameter controls without feature-position controls;
- room-temperature dimensions without relevant operating conditions;
- a tolerance with no defined inspection method;
- “100% inspection” without identifying the inspected characteristics.
A numerical tolerance has meaning only when the feature, Ngày, Tiêu chuẩn, conditions, and measurement method are clear.
Verify the Pin, Hole, Pattern, and Assembly
Inspection should follow the structure of the specification.
| Yêu cầu được kiểm soát | Hướng xác minh phù hợp |
| Đường kính pin | Đo tại các vị trí và hướng xác định |
| Đường kính lỗ hoặc ống lót | Xác minh giới hạn lỗ khoan bằng phương pháp hiệu chuẩn thích hợp |
| Vị trí chốt hoặc lỗ | Đo lường so với khung tham chiếu dữ liệu đã nêu |
| Hướng trục | Xác minh mối quan hệ vuông góc hoặc góc |
| Khoảng cách mẫu | Đo lường mối quan hệ giữa các đối tượng địa lý định vị |
| Tương tác hoàn chỉnh | Sử dụng kiểm tra lắp ráp có kiểm soát hoặc máy đo chức năng nếu thích hợp |
| Độ lặp lại | Kiểm tra lắp ráp lặp lại trong các điều kiện xác định |
No single measurement verifies every requirement.
A micrometer may confirm a pin diameter but cannot establish the pin’s position in the mold plate. A bore measurement may confirm hole size but not perpendicularity. A functional gauge may show that the current assembly engages, but it may not identify which individual feature is approaching its tolerance limit.
The inspection plan should also consider:
- instrument resolution;
- trạng thái hiệu chuẩn;
- sự cố định;
- measurement temperature;
- accessibility of the feature;
- measurement uncertainty.
If the measurement uncertainty is too large relative to the tolerance, the conformity decision becomes unreliable. Component conformity also does not automatically prove long-term repeatability under heat, mặc, and repeated mold cycles.
Quyết định xem thành phần tiêu chuẩn hay dung sai tùy chỉnh là cần thiết
A standard pin or bushing is suitable when its published dimensions, lớp dung sai, hình học, Vật chất, and mounting configuration satisfy the calculated tolerance stack.
Customization may be justified when the design requires:
- a non-standard diameter or locating length;
- separate mounting and locating diameters;
- vai hoặc mặt bích đặc biệt;
- a defined relieved-pin orientation;
- a specific material or hardness;
- a controlled surface finish;
- unusual retention or removal features;
- a tolerance not available in a standard series.
The decision should start with the functional requirement rather than an assumption that custom parts are automatically more precise. A custom pin still depends on the mating hole, bushing, Hệ thống ngày tháng, và phương pháp kiểm tra.
SunshinePro states that it supplies mold components and supports non-standard accessories based on drawings or samples. Nó định vị ống lót dẫn hướng pin page lists straight, có mặt bích, and custom structures, along with standard or customized sizes. Buyers comparing catalog and drawing-based options can also review the broader guidance on Các bộ phận tiêu chuẩn khuôn.
Trước khi đặt hàng, confirm which feature the supplier’s stated tolerance applies to, how it will be inspected, and whether the component must be interchangeable with other pins or bushings.
For a drawing-based review, provide the pin and mating-feature limits, datum scheme, độ vừa vặn bắt buộc, điều kiện vận hành, material or hardness requirements, and inspection expectations through the Trang liên hệ SunshinePro.
Chia sẻ:



Được viết bởi Sunshine
Tại Sunshine, Chúng tôi là nhà sản xuất và cung cấp chuyên nghiệp các linh kiện khuôn chính xác, cung cấp một loạt sản phẩm đa dạng cho ứng dụng dập và khuôn ép. Trọng tâm chính của chúng tôi bao gồm khuôn đục lỗ, ghim và ống lót đẩy, và cọc hướng dẫn cùng các bushing. Với gia công CNC tiên tiến, Kiểm soát chất lượng nghiêm ngặt, và năng lực sản xuất mạnh mẽ, chúng tôi đảm bảo độ tin cậy, các bộ phận chính xác cao, cùng với các linh kiện tiêu chuẩn có sẵn trong kho để cung cấp nhanh chóng và hiệu quả toàn cầu.
TIN TỨC
NHẬN DỊCH VỤ
Với các bộ phận chất lượng đáp ứng mọi ngân sách và đội ngũ nhân viên thân thiện được đào tạo để giúp chuyến thăm của bạn trở nên hữu ích và thuận tiện.
